Premium conveyor systems, components, and idler brackets manufactured to international standards
In modern high-capacity logistics and mining infrastructure, steel cord conveyor belts represent the peak of bulk handling capability. Heavy industries are operating at unprecedented scales, requiring systems that can transport massive tonnages across challenging topography, over miles of mountainous or underground environments. Steel cord core design provides the extremely high tensile strength and minimal structural elongation necessary for these operations.
Global demand continues to grow in mineral extraction (iron ore, copper, gold), bulk shipping ports, coal-fired power plants, and modern dry-process cement facilities. These applications require dynamic strength, impact resistance, and long-term durability. Traditional fabric ply belts can experience elongation and splice failures over long distances, whereas steel wire rope reinforcement provides reliable operational continuity under high mechanical tension.
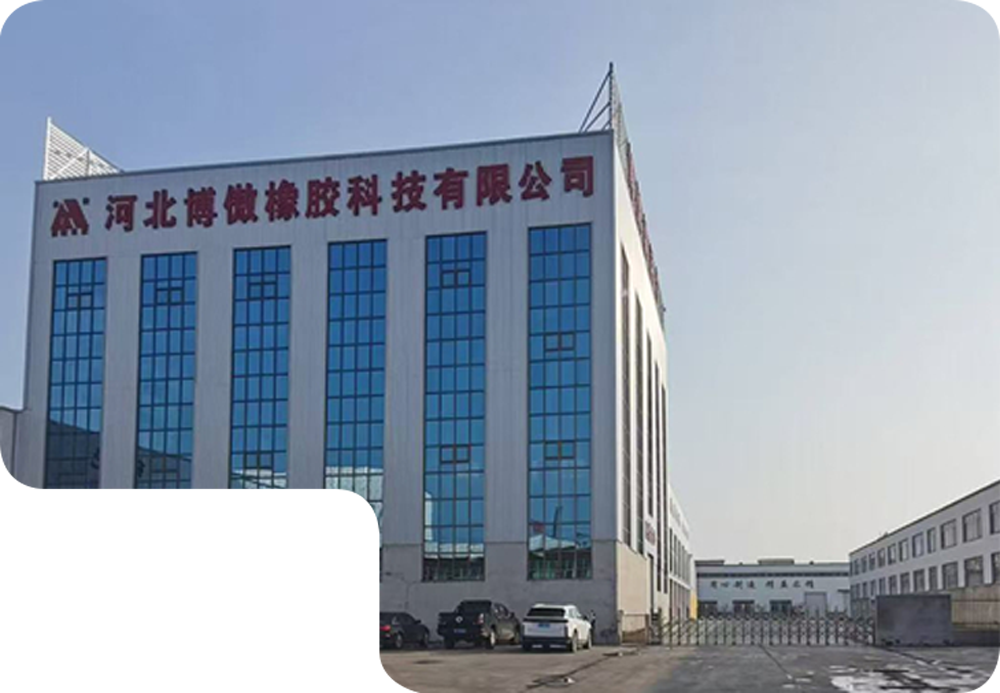
Established in 2004, Hebei Boao Rubber Technology Co., Ltd. has developed advanced industrial polymer and steel cord integration systems for over two decades.
A deep dive into our manufacturing infrastructure and commitment to quality engineering
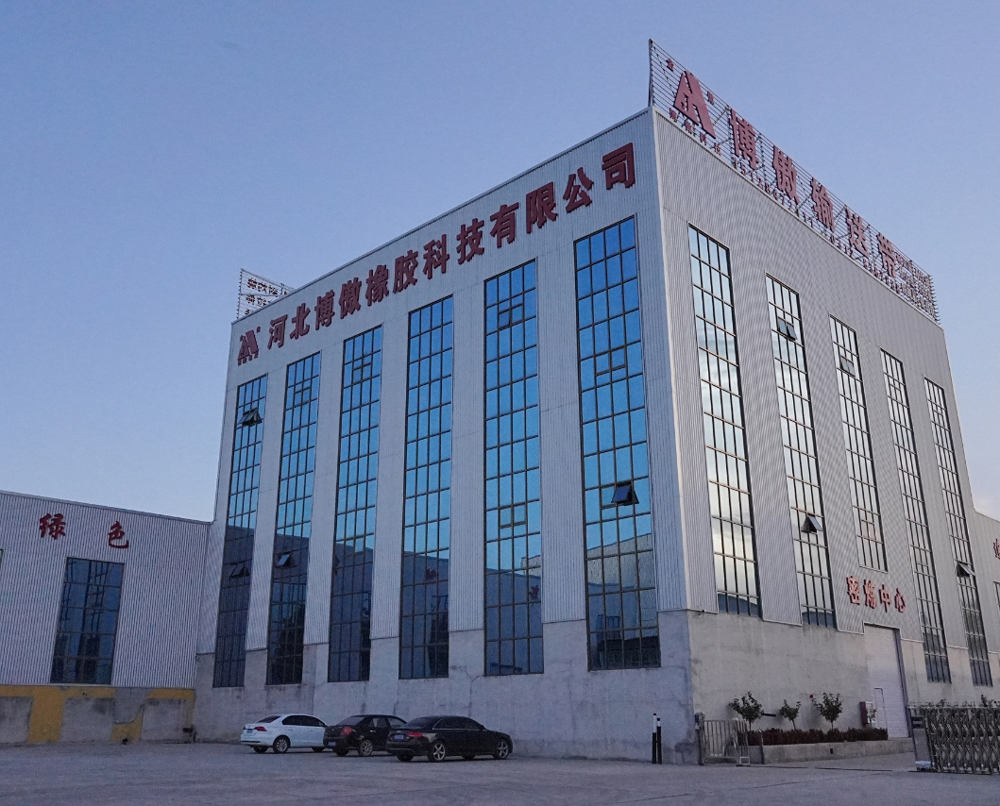
Hebei Boao Rubber Technology Co., Ltd. is located in the Rubber Industrial Park of Boye County, Baoding, Hebei Province. The company covers an area of over 30 acres. Our registered brand, "Jinao", is recognized for reliable engineering components, high-tensile multi-ply belts, and impact-resistant idler systems.
We are a professional manufacturer in China that integrates product development, research, design, manufacturing, and business services for conveyor belts and conveyor machinery accessories. We have passed the international quality management system certification. Our production lines feature advanced rolling, forming, vulcanization, and material testing systems that process products from raw compound to finished conveyor configurations.
Our quality assurance system features testing equipment that measures compounds, wire rope tension, and adhesive properties to maintain consistency across production runs.
Technical expertise and strict quality control systems at the core of our operations
Our facility features an independent chemical analysis laboratory and physical testing facility. We monitor key points from raw material selection to final vulcanization and curing. Materials that do not meet specification are not processed, and finished products undergo testing before shipping.
Our quality control program utilizes trained technicians and testing equipment to evaluate mechanical performance parameters. We run tests for steel cord adhesion, cover compound abrasion resistance (DIN standard limits), and tensile strength retention after aging.
Supported by engineering services and post-sales support networks, our products are distributed across industrial centers in China and international markets. Our conveyor belts and components are used in steel manufacturing, metallurgy, underground coal mining, cement works, power stations, ports, and fertilizer storage sites.
Our vulcanization process integrates heat and pressure control to achieve consistent properties. For steel cord belts, maintaining precise alignment and uniform tension of individual wire ropes during the rubber injection and curing stage is critical. Our production equipment manages this process, which helps prevent tracking issues, belt distortion, and uneven stress distribution under heavy loads.
Comprehensive bulk handling solutions, from high-performance belt designs to custom support components
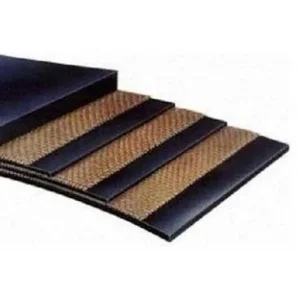
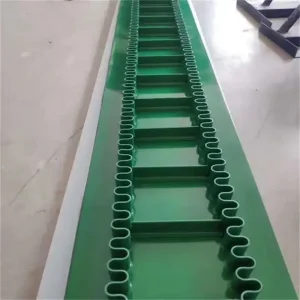
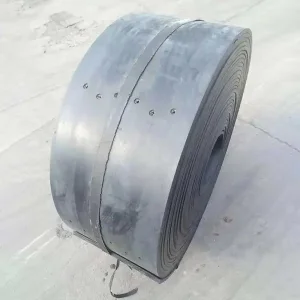
We manufacture a wide range of conveyor belt designs optimized for specific industrial applications:
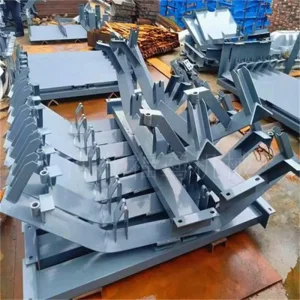
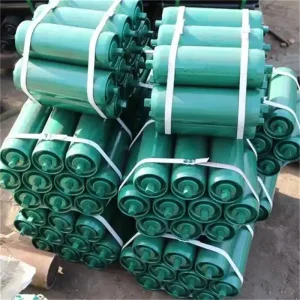
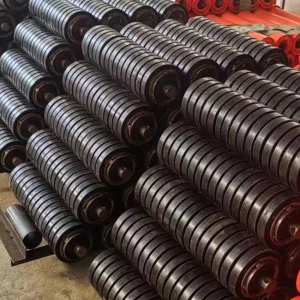
To support belt operations, we produce matching components that help optimize conveyor system performance:
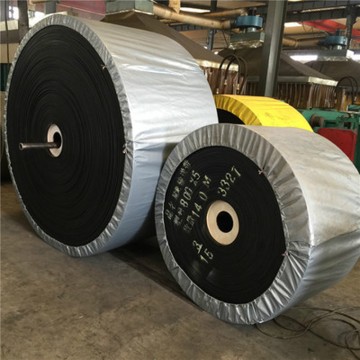
Specifically formulated to withstand continuous temperatures up to 200°C in cement and metallurgical transport lines.
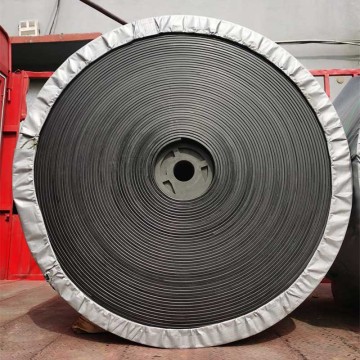
Maintains elastic properties and prevents cracks in extreme winter conditions down to -50°C.
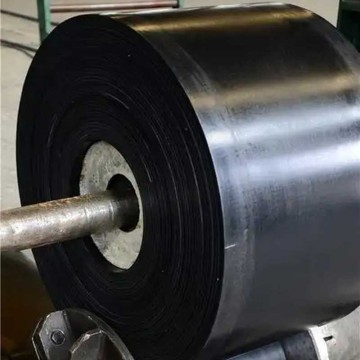
EP/NN core with cover compounds designed for chemical plants, fertilizer facilities, and paper mills.
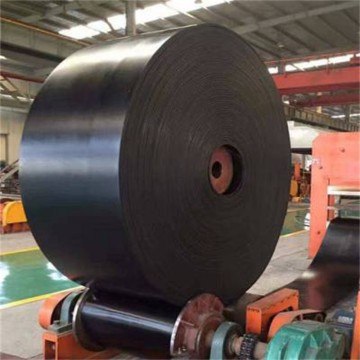
Features high wear resistance, high tensile strength, and impact absorption properties.
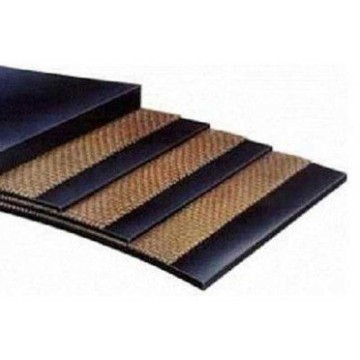
Reliable daily transport solution for aggregates, sand, coal, and dry cement materials.
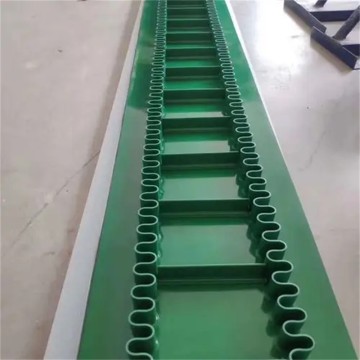
Clean-running option for package handling, food processing, and general light industrial lines.
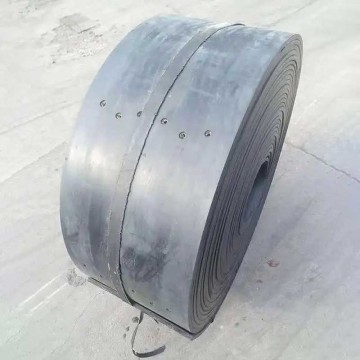
Highly reinforced vertical transport solution designed for bucket elevator systems.
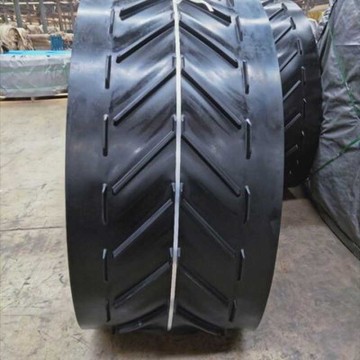
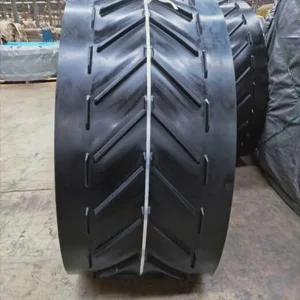
V-cleat and multi-chevron designs to prevent materials from sliding back on high-incline conveyors.
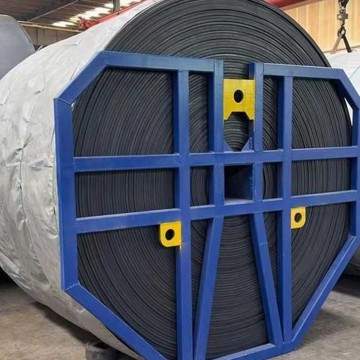
Features integrated transverse steel cords or high-strength breaker fabric to prevent longitudinal slitting.
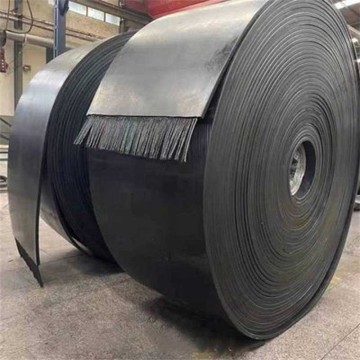
Engineered for high-tension, long-distance industrial overland bulk transport systems.
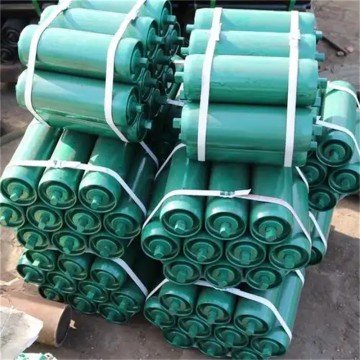
Flexible garland structures that conform to heavy loads, helping to minimize frame stress.
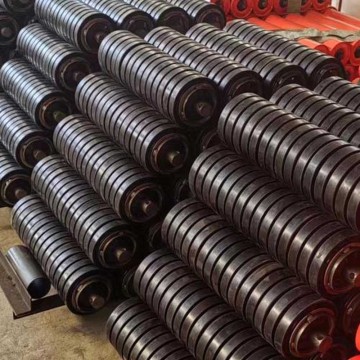
Heavy rubber rings mounted on steel tubing to absorb material impact at loading chutes.
Delivering high-tensile conveying solutions for heavy industries and infrastructure projects
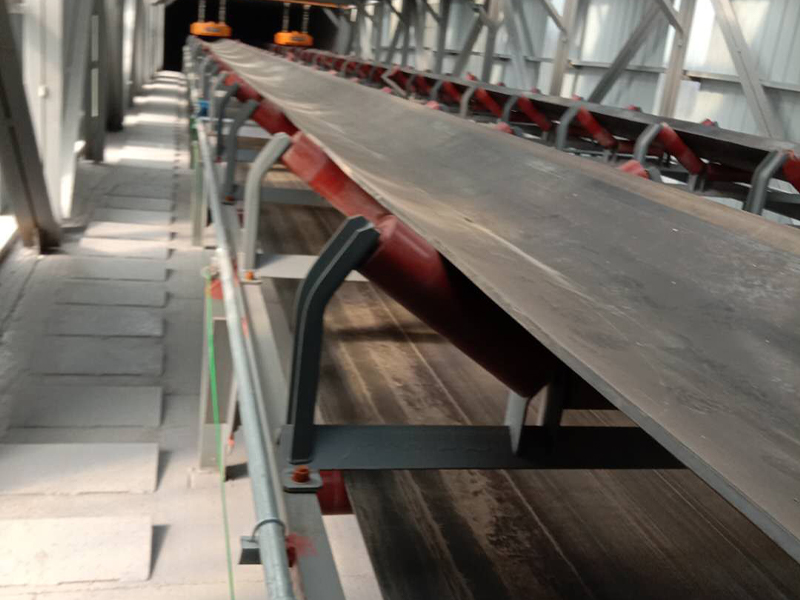
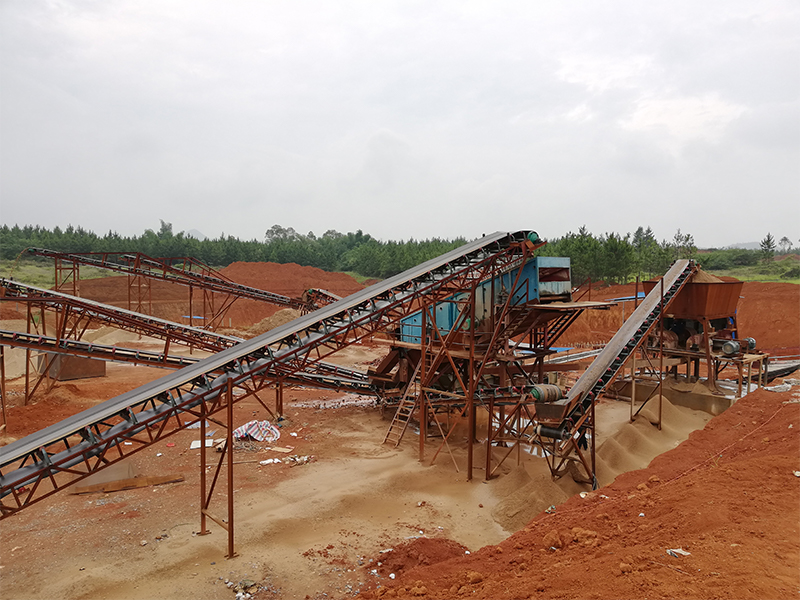
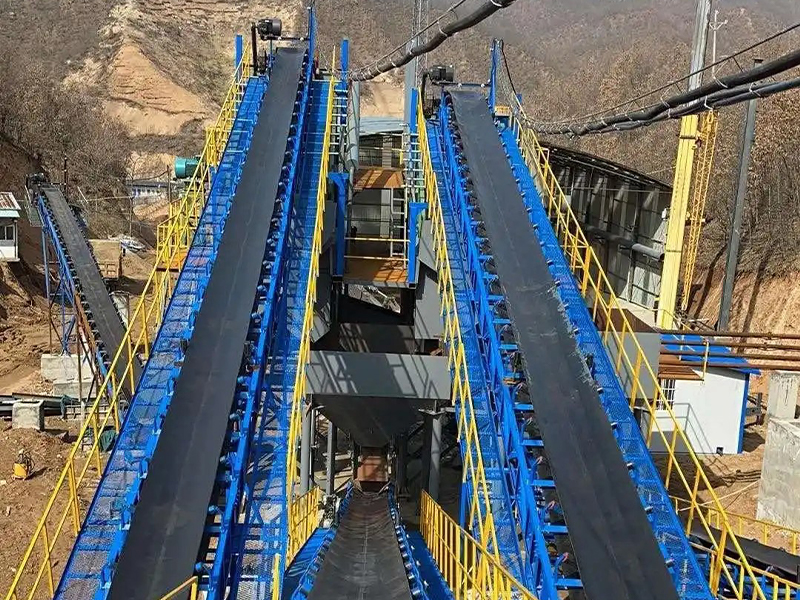
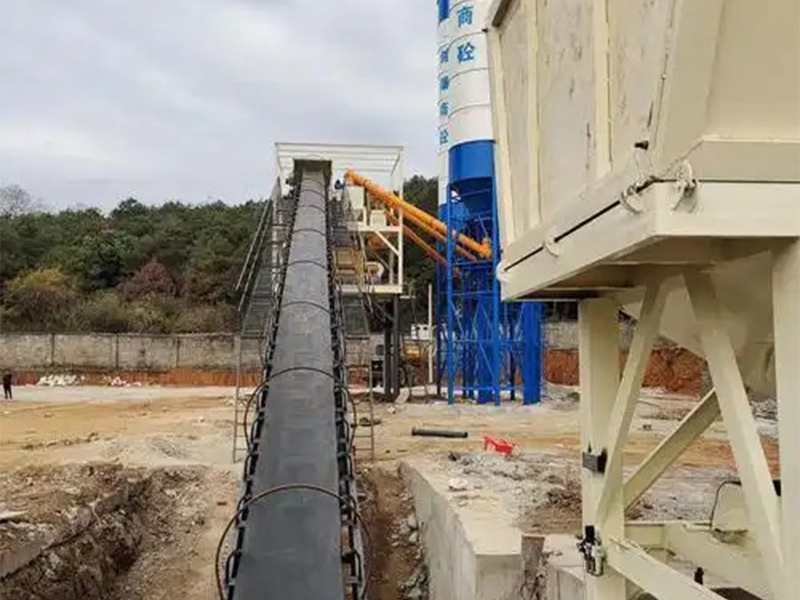
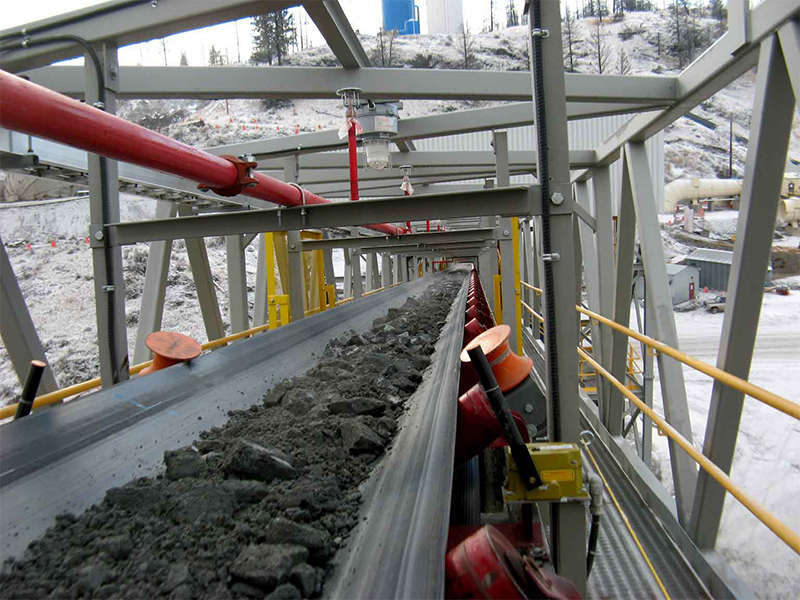
Our conveyor belts and components are used across different industrial sectors. By matching rubber formulations to specific operational requirements (such as oil-resistant, high-temperature, or flame-retardant needs), we provide solutions that support the performance of heavy industrial transport networks.
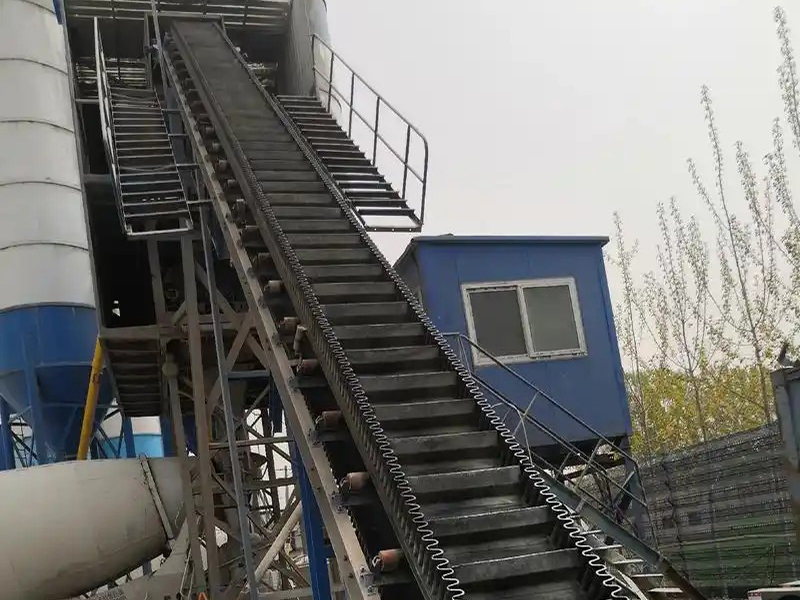
Extending equipment lifetime and optimizing plant runtime through end-to-end support
Our engineering services include planned replacement, mechanical repair, routine inspections, scheduled maintenance, and emergency response. We work to support system availability and reduce downtime in critical production lines.
Our scope of work covers the supply of conveyor belts and replacement rubber materials, maintaining recommended safety stock levels, managing inventory storage conditions, vulcanized splice bonding, cover repair, regular belt profiling, and system checks.
We focus on improving belt system runtime, managing belt wear, and supporting operational efficiency. We cooperate with plant managers to help extend belt service life and align maintenance intervals with production schedules.
In the modern industrial landscape, rubber conveyor belts have become the backbone of bulk material transport systems across multiple sectors. From mining operations extracting raw materials from deep underground to port facilities handling millions of tons of cargo annually, heavy-duty rubber belts facilitate the seamless movement of materials that power our global economy. The evolution of these critical components reflects decades of engineering innovation, material science breakthroughs, and an unwavering commitment to operational efficiency and safety.
Verified manufacturing processes and compliance with international standards
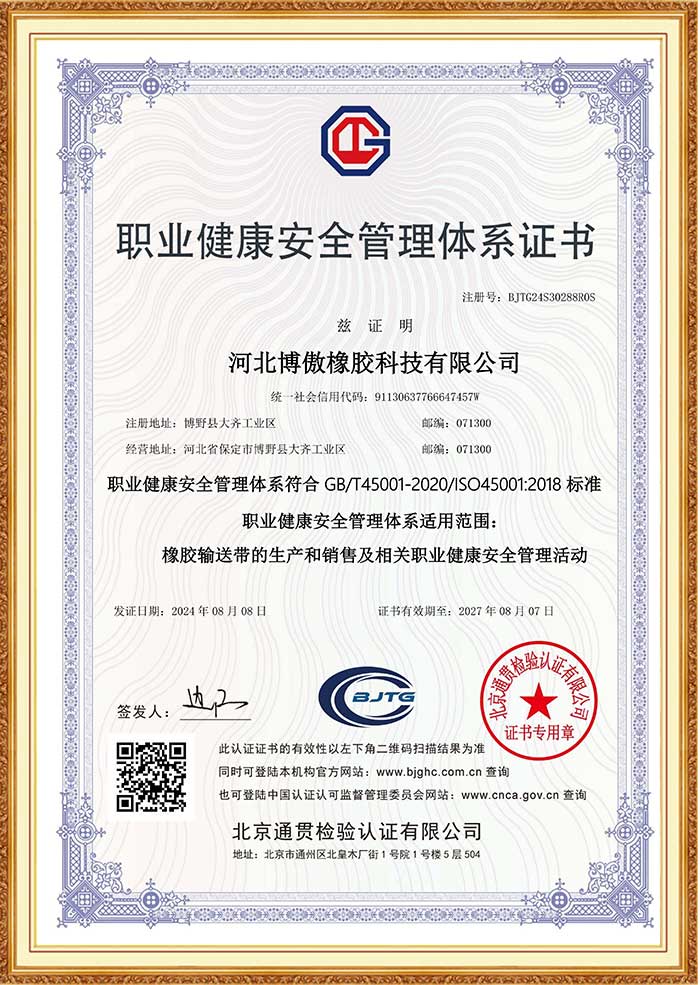
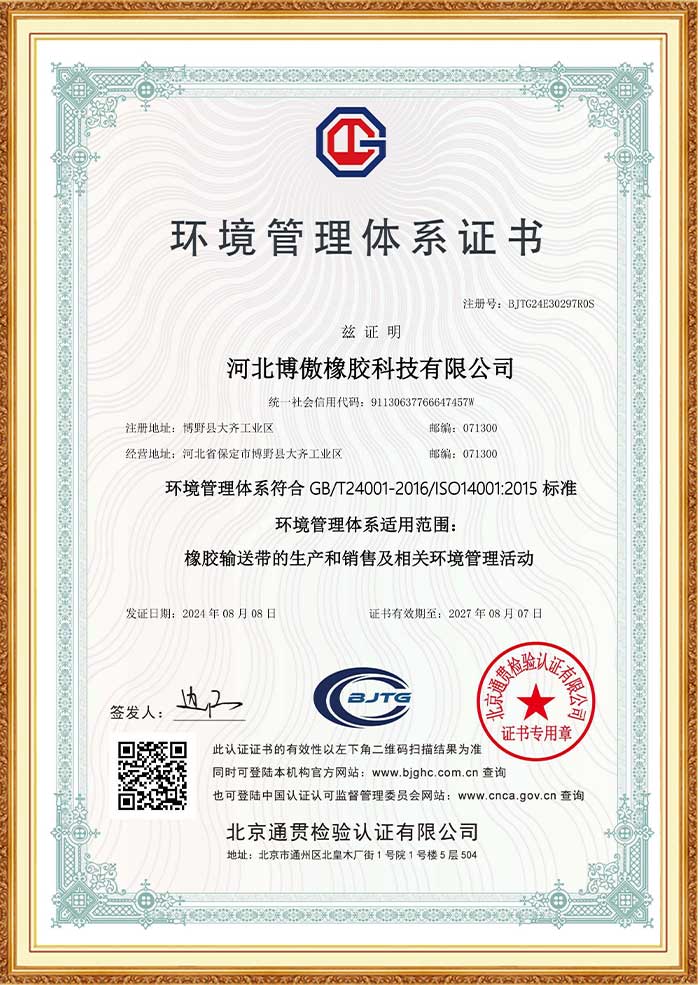
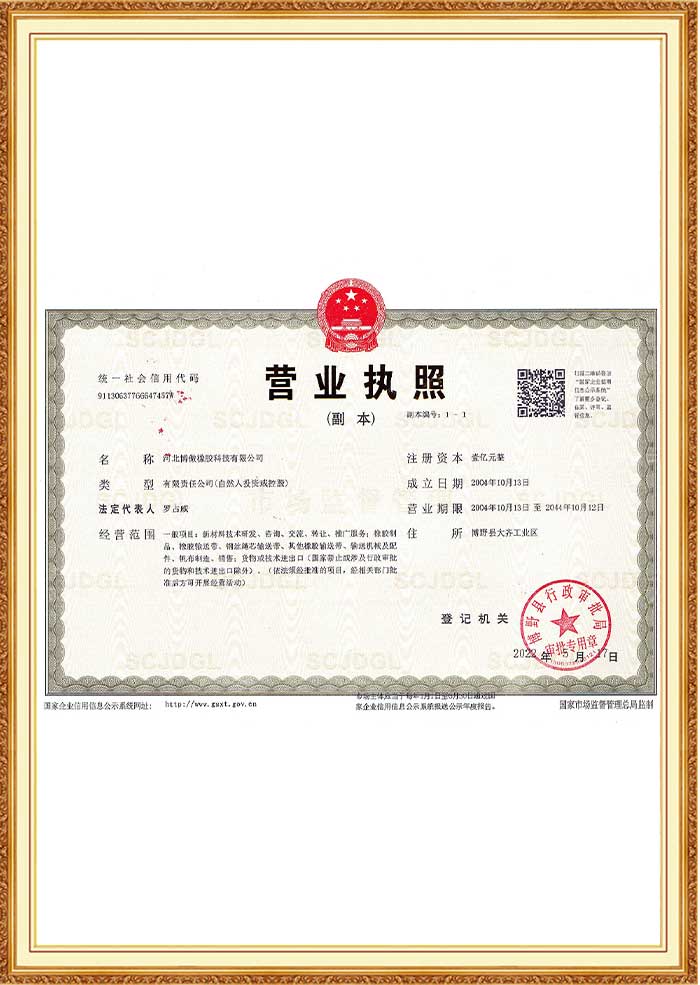
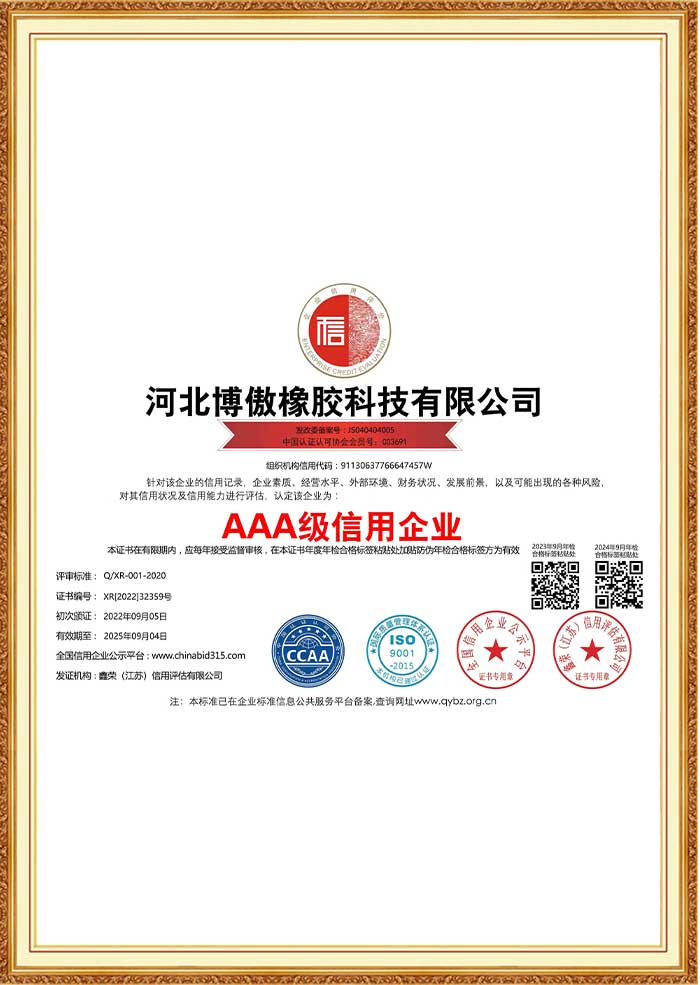
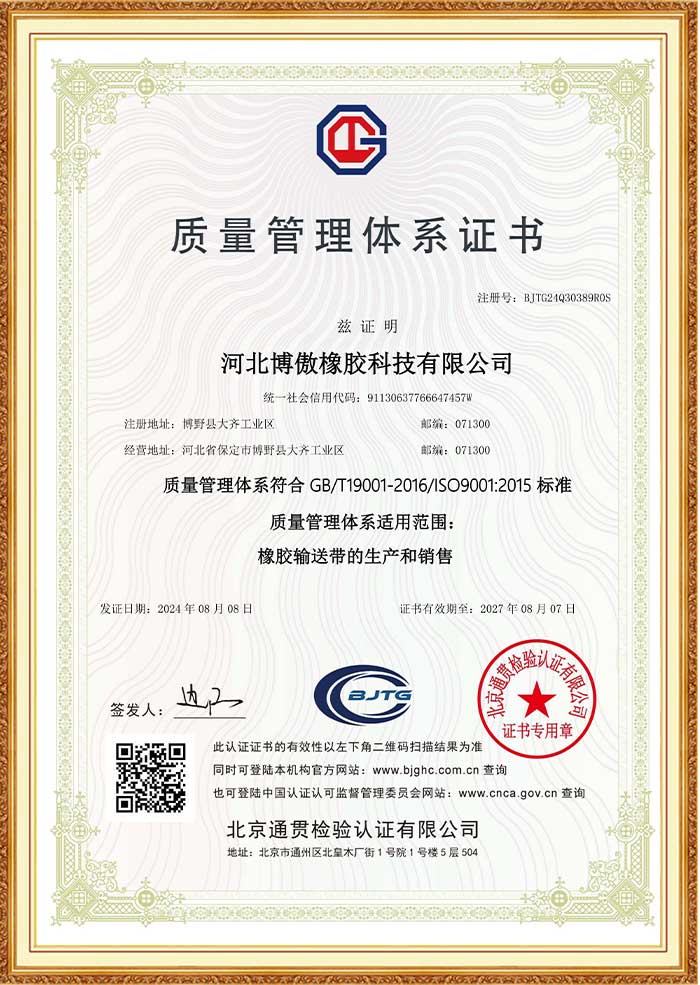
To build customer confidence in the reliability of our products, Hebei Boao Rubber Technology Co., Ltd. maintains certification under standard quality management systems.
Expert technical insights regarding selection, installation, and operation of steel cord and fabric rubber belts
Browse our selection of specialized industrial belts and tracking idler structures
We are committed to providing you with quality products and support services. If you have questions or require assistance with our conveyor belts, component designs, or custom configurations, please reach out to our team.
Inquiry Now Boao Rubber