Optimized bulk material handling components built for extreme durability and precise operational alignment.
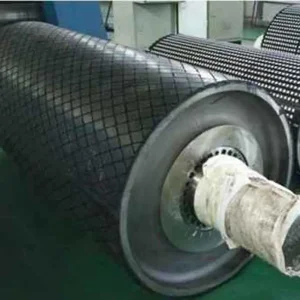
High-performance trough-type idler rollers engineered to reduce belt wear and ensure smooth tracking in high-capacity Annaba processing lines.
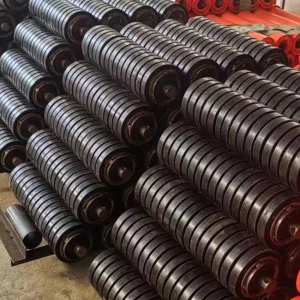
Shock-absorbing impact idlers designed to cushion heavy ore drops and safeguard structural belts at loading transfer points.
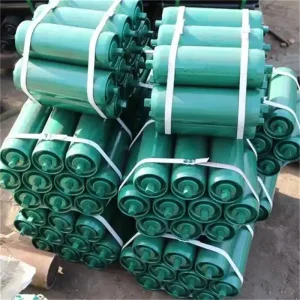
Flexible suspended trough-shaped roller assemblies built to accommodate uneven terrain and heavy dynamic loads in industrial plants.
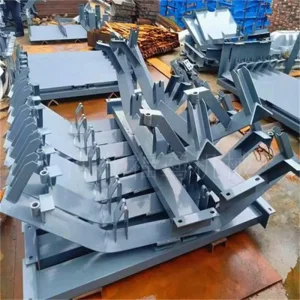
Precision-bearing idler rollers offering superior load capacities, minimal rotational resistance, and extended service intervals.
Strategic insights into bulk material transport, regional industrial evolution, and high-performance component engineering.
Hebei Boao Rubber Technology Co., Ltd. delivers world-class industrial infrastructure, backed by rigorous research, development, and stringent quality protocols.
Annaba stands as a premier industrial powerhouse in North Africa, anchored by heavy metallurgy, mineral processing, port logistics, and extensive chemical manufacturing. As a major maritime hub and industrial gateway, enterprises in Annaba demand robust bulk material handling solutions capable of withstanding corrosive coastal environments, abrasive iron ores, and continuous heavy-duty operational cycles. Conveyor downtime directly impacts regional production output, making the integration of high-grade rubber belts, precision idler rollers, and wear-resistant accessories an absolute economic necessity.
Local industrial facilities, ranging from steel complexes to fertilizer plants and port terminals, require supply partners who understand the unique climatic and mechanical stresses of the region. High ambient temperatures, airborne particulate matter, and salt-laden coastal air necessitate specialized corrosion-resistant components and flame-retardant belting solutions that comply with international safety standards.
In the modern industrial landscape, rubber conveyor belts have evolved from simple transit bands into sophisticated, high-tensile conduits of global commerce. From underground mining operations extracting raw minerals to automated port facilities handling millions of tons of cargo annually, heavy-duty belts facilitate the seamless movement of materials that power economies worldwide.
The evolution of these critical components reflects decades of engineering innovation, material science breakthroughs, and an unwavering commitment to operational safety. Modern developments include steel wire rope core designs for ultra-long-distance overland transport, multi-ply nylon (NN) and polyester (EP) fabrics for high tensile strength with low elongation, and specialized compound covers resistant to extreme heat, oils, acids, and flame combustion.
Looking toward the future, the conveyor accessories industry is rapidly embracing smart manufacturing principles and predictive maintenance technologies. Key development vectors include:
1. IoT-Enabled Smart Idlers: Integration of embedded vibration and thermal sensors within idler roller bearings to monitor real-time wear and prevent catastrophic mechanical failures.
2. Eco-Friendly & Energy-Efficient Compounds: Utilization of low-rolling-resistance rubber formulations that significantly reduce electrical energy consumption in long overland conveyor layouts.
3. Advanced Composite Materials: Adoption of high-durability polymers and ceramic-coated impact plates to maximize lifespan in severely abrasive ore-handling applications.
Founded in 2004 and situated in the Rubber Industrial Park of Boye County, Baoding, Hebei Province, Hebei Boao Rubber Technology Co., Ltd. spans over 30 acres of advanced manufacturing facilities. Operating under our renowned brand "Jinao", we function as a premier integrated manufacturer specializing in product research, design, precision fabrication, and professional commercial services for conveyor belts and machinery accessories.
Our operational infrastructure features state-of-the-art production lines dedicated to calendering, forming, vulcanization, and rigorous laboratory material testing—ensuring flawless quality control from raw polymer compounds to finished industrial goods. We have successfully achieved international quality management system certifications, cementing our reputation as a trusted global exporter.
Our commitment to absolute reliability is validated by comprehensive national and international quality standards:
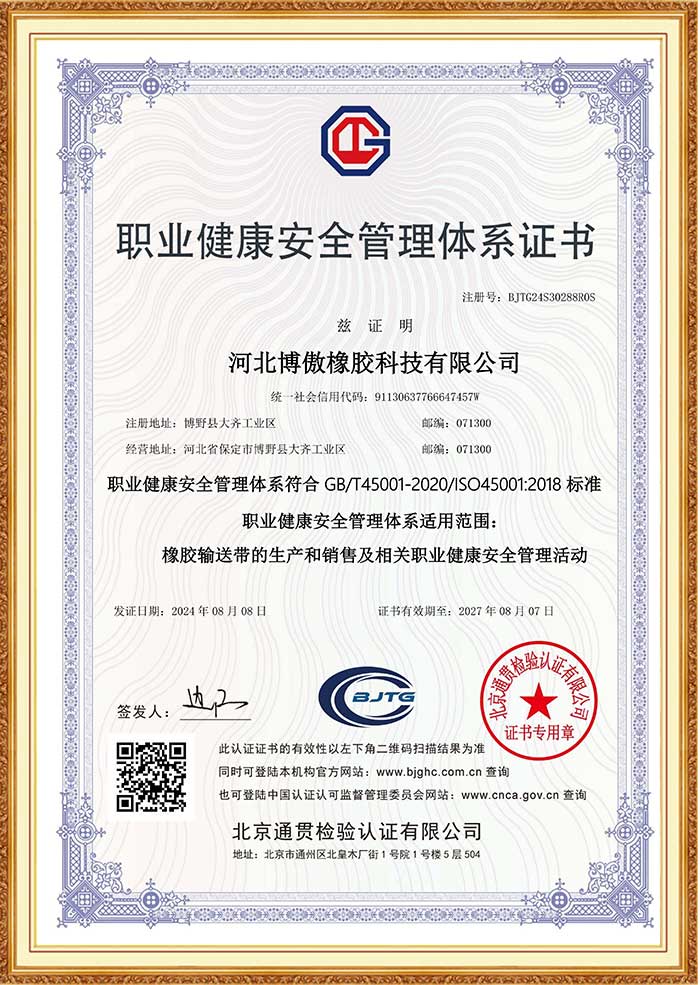
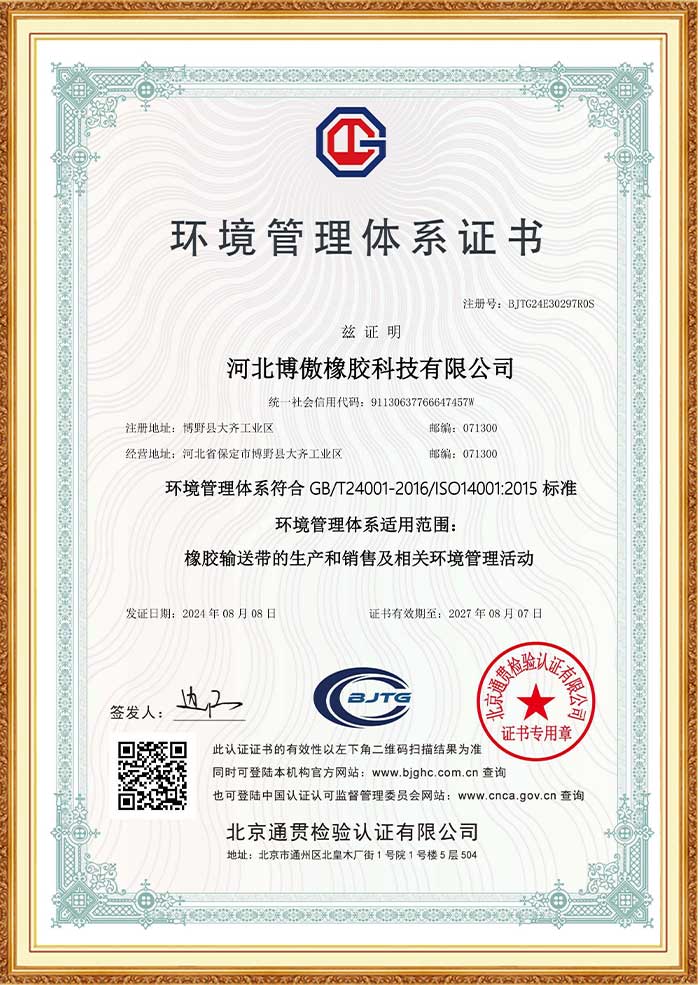
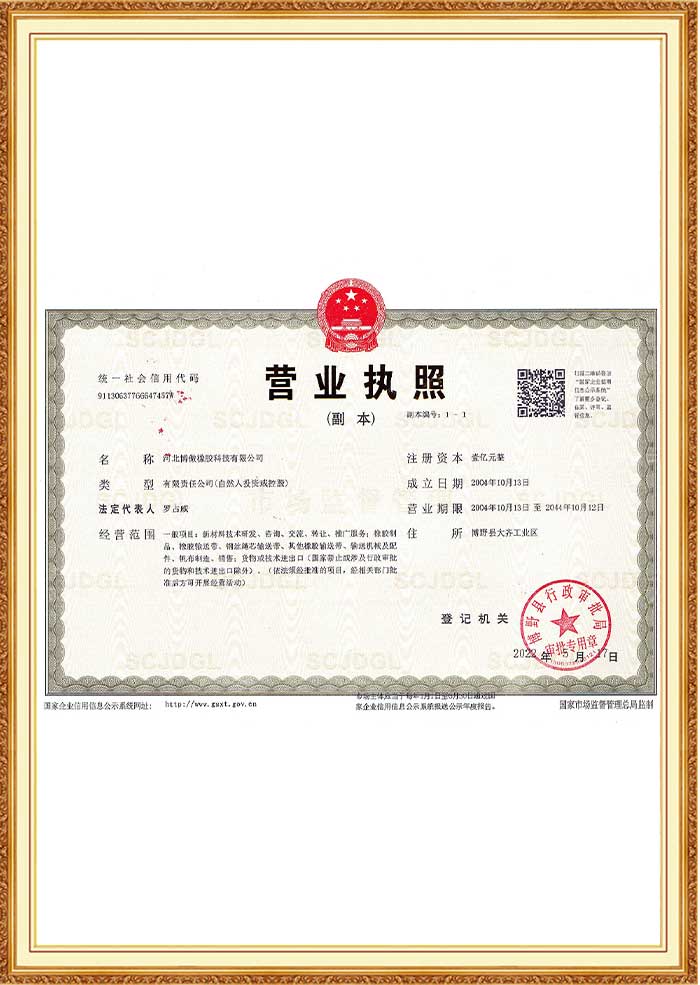
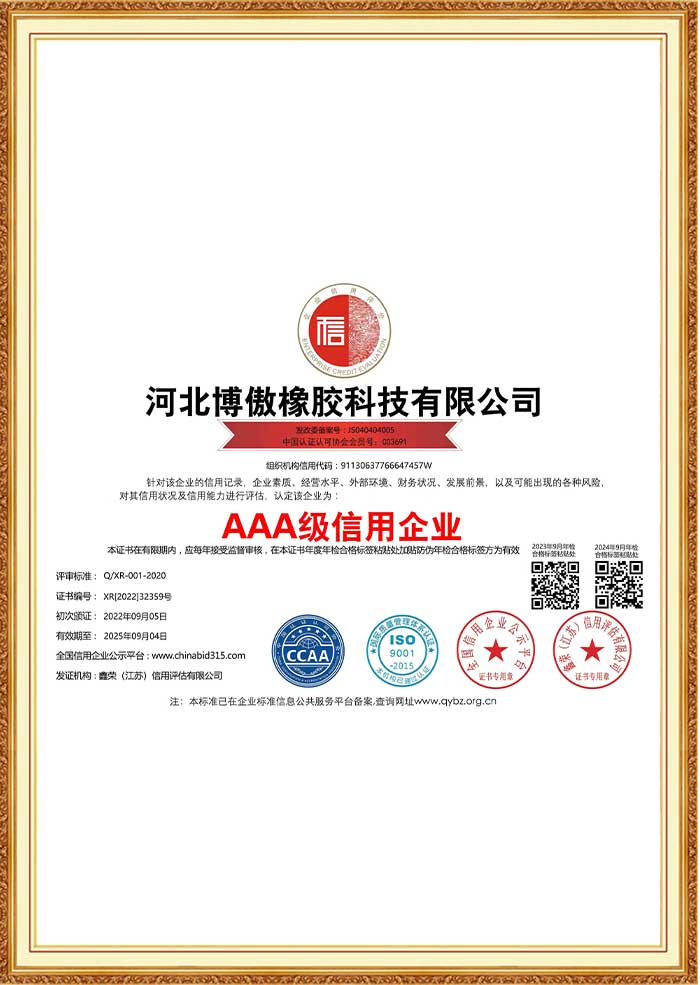
Skip the hassle of sourcing from multiple suppliers – our factory provides your ideal industrial packaging and material transport solutions all in one place.
Comprehensive planned replacement, expert repair, rigorous periodic inspection, routine maintenance, and swift emergency repair of all conveyor belt systems.
Supply of high-grade conveyor belts and raw rubber materials, safety stock guarantees to prevent operational bottlenecks, daily inventory storage, professional vulcanized splicing, and surface maintenance.
Maximize belt conveyor operational efficiency, reduce wear consumption, extend equipment lifecycles, and achieve a mutual, sustainable win-win partnership.
Proven reliability in heavy industries worldwide, from major railway infrastructure to leading cement and mining conglomerates.
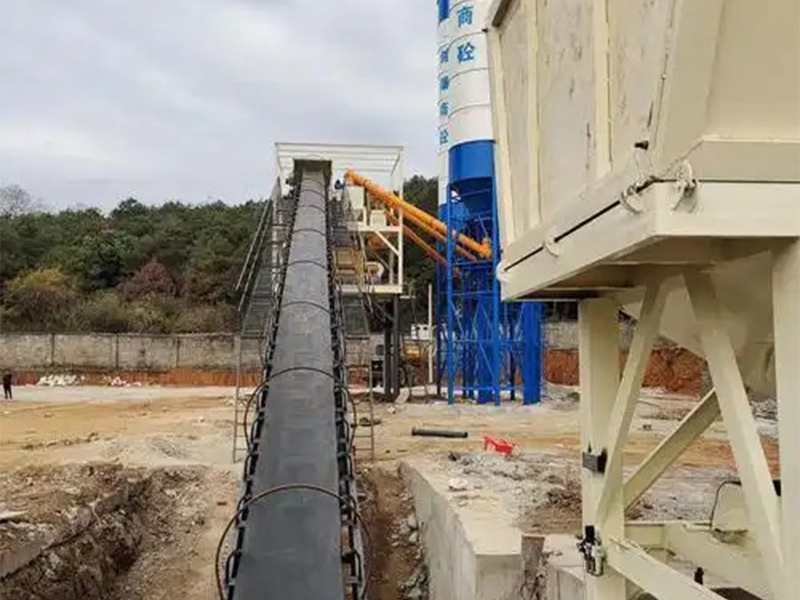
Heavy-duty transport belts ensuring reliable aggregate feeding for high-speed rail construction.
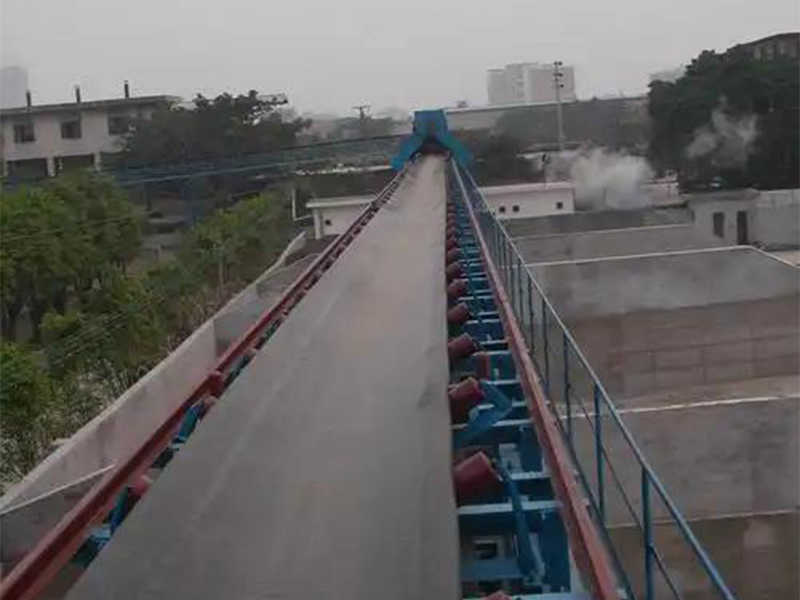
Heat-resistant conveyor solutions engineered for clinker transport in cement manufacturing.
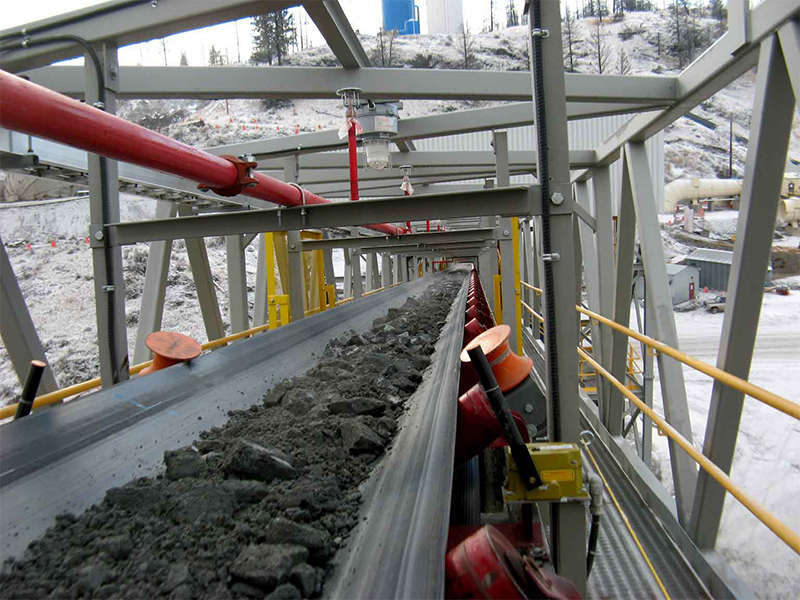
Flame-retardant and high-strength belts supporting deep underground coal extraction.
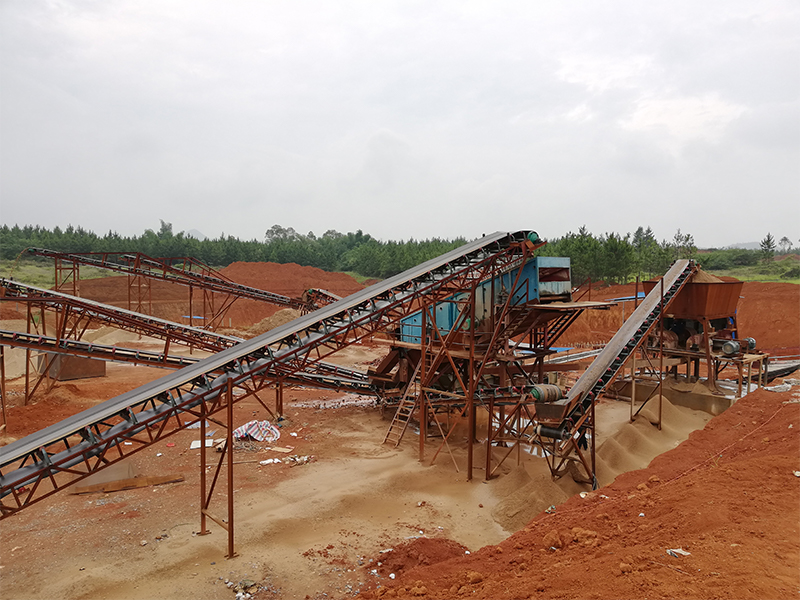
Corrosion-resistant roller assemblies and belts for metallurgical processing operations.
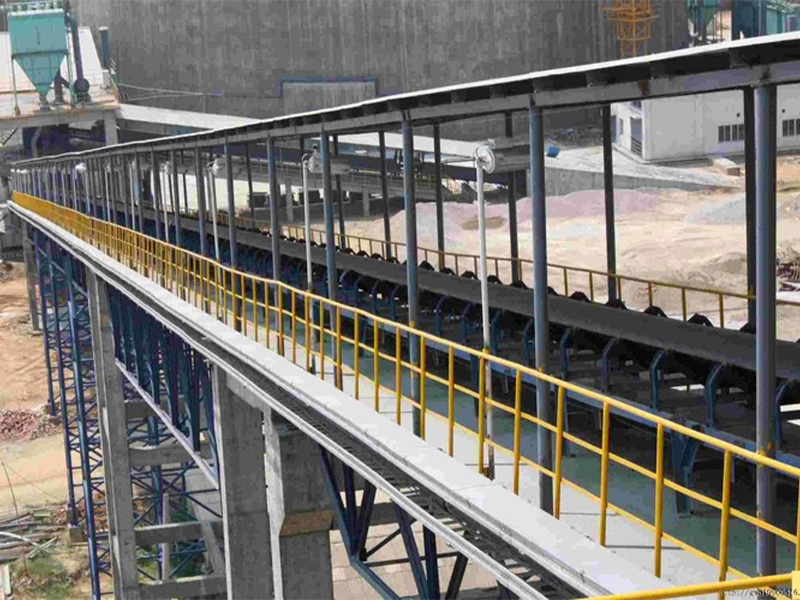
Long-lasting abrasion-resistant rubber conveyor lines for continuous kiln feed systems.
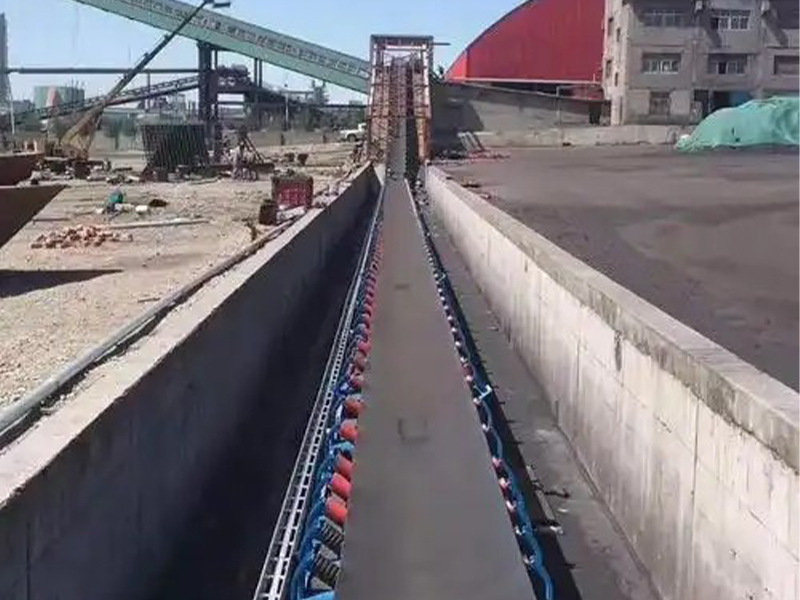
High-tension steel wire rope core belts designed for high-capacity overland haulage.
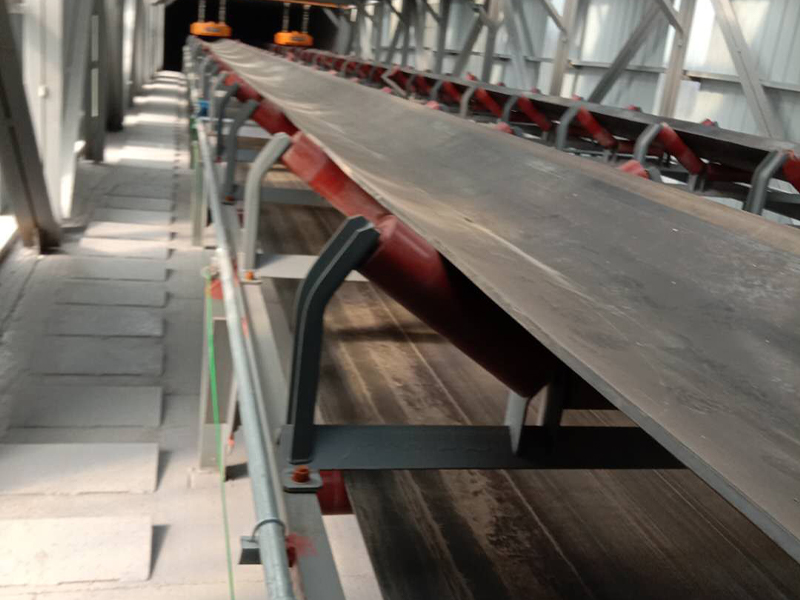
Rugged idler roller arrays built to withstand extreme mechanical shock in steel mills.
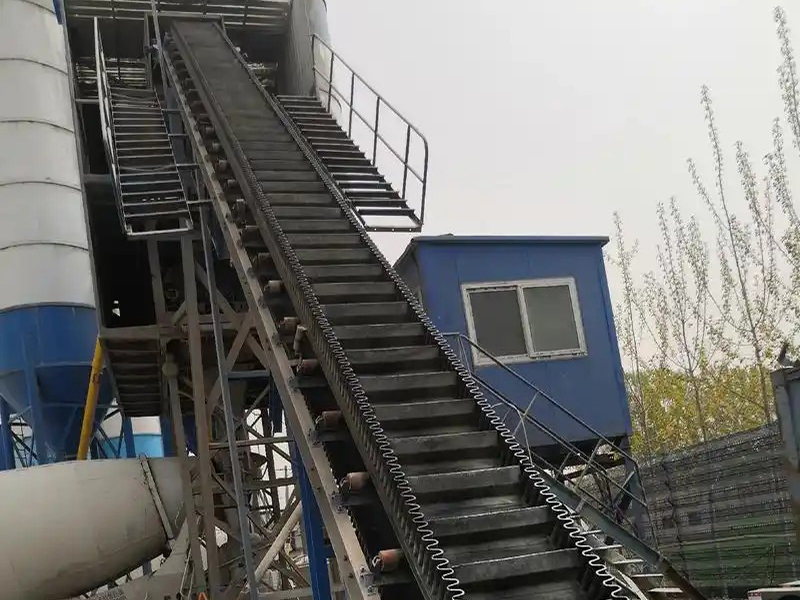
Precision-engineered replacement rollers and multi-ply belts for uninterrupted heavy metallurgy.
Expert answers regarding product selection, shipping to Annaba, custom specifications, and industrial standards.
For Annaba's corrosive coastal and heavy metallurgical environments, we recommend steel wire rope core conveyor belts for high-tension overland transport, flame-retardant rubber belts for safety-critical facilities, and heat-resistant EP/NN belts for high-temperature material processing.
Our products utilize premium quality rubber compounds formulated with high tear-resistance and tensile strength. Our idler rollers feature precision deep-groove ball bearings and multi-labyrinth sealing systems to prevent dust and moisture ingress.
Yes, as a direct manufacturer with over 22 years of production experience, we offer comprehensive OEM/ODM customization for roller diameters, lengths, bracket configurations, and custom belt tensile ratings to match your exact specifications.
We maintain robust safety stock and efficient export logistics. Standard stock items ship promptly, while custom manufacturing orders are expedited to ensure minimal downtime for your regional industrial operations.
Explore our full range of certified industrial conveyor components engineered for maximum efficiency and longevity.
High-Quality Conveyor Trough-Type Idler Rollers designed for efficient material handling across diverse industrial settings.
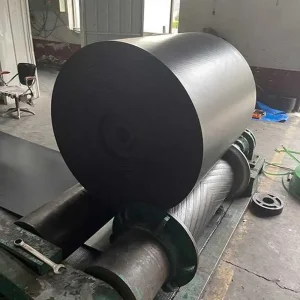
Best Flame Retardant Rubber Conveyor Belt manufactured for safety-critical mining and industrial applications.
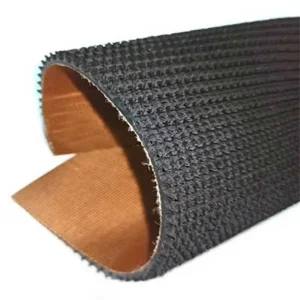
China Patterned Conveyor Belt engineered for inclined bulk transport with superior grip and material retention.
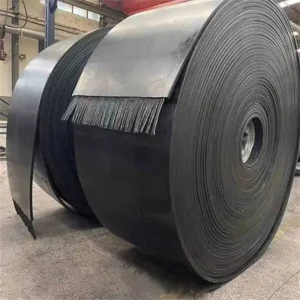
China Steel Wire Rope Core Conveyor Belt Suppliers providing high-quality factory products for heavy-duty transport.
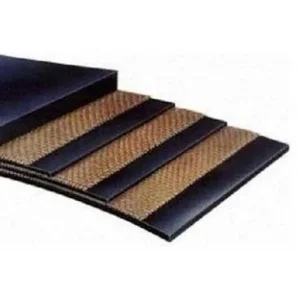
China General-Purpose Rubber Conveyor Belt quality factory suppliers optimized for general bulk material handling.
China Suppliers Factory Rubber Buffer Idler Roller built for corrosive environments in mining and processing.
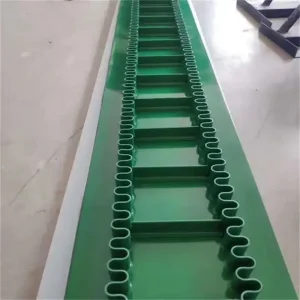
Best PVC-PU Lightweight Conveyor Belt quality China supplier & factory for durable, clean material solutions.
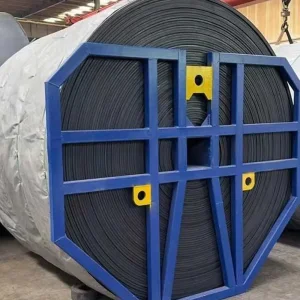
Best High-Quality Anti Tear Steel Wire Rope Core Conveyor Belt from China suppliers for safe material transport.
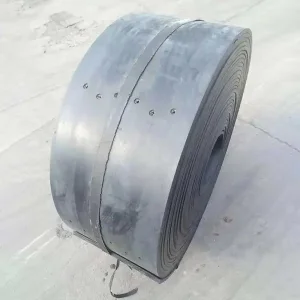
China Rubber Lifting Conveyor Belt Suppliers delivering high-quality industrial factory products for bucket elevators.
China General-Purpose Rubber Conveyor Belt reliable suppliers and factory partners for bulk material handling.
China Flame Retardant Rubber Conveyor Belt Manufacturer offering certified fire-resistant factory products.
China Suspended Rollers Of The Conveyor Belt Machine in a trough shape supplier and factory direct solutions.
Partner with Hebei Boao Rubber Technology Co., Ltd. for factory-direct pricing, custom engineering support, and reliable global delivery.
Send Inquiry Now Boao Rubber