Explore our core manufacturing line engineered for extreme durability and optimal bulk material performance.
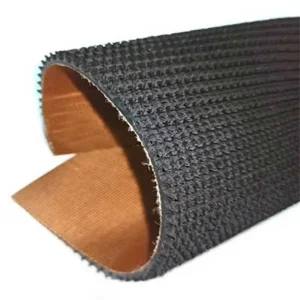
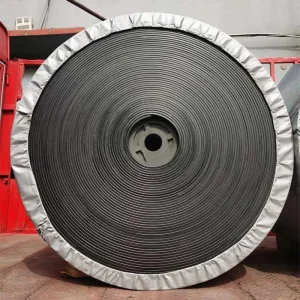
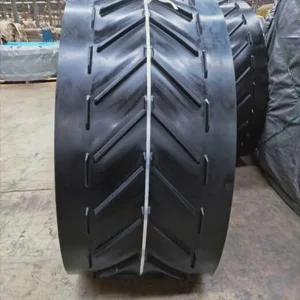
Hebei Boao Rubber Technology Co., Ltd. is located in the strategic Rubber Industrial Park of Boye County, Baoding, Hebei Province. Founded in 2004, our enterprise covers an expansive area of over 30 acres, establishing a robust industrial manufacturing base dedicated to world-class material transmission solutions.
Under our prestigious product brand "Jinao", we operate as a premier manufacturer in China integrating product research, innovative design, advanced engineering, full-scale manufacturing, and professional business services for conveyor belts and associated machinery accessories. Having successfully passed international quality management system certifications in a single audit, our facility houses state-of-the-art automated production lines for rolling, precision forming, high-temperature vulcanization, and stringent rubber testing—ensuring uncompromising quality control from raw chemical inputs to finished industrial goods.
Rigorous quality assurance, accredited testing methodologies, and expansive industry deployment across heavy sectors.
Our independent chemical analysis room and physics laboratory conduct ongoing chemical and mechanical tests. We strictly follow zero-tolerance protocols: unqualified raw materials never enter our site, and substandard products never leave.
Staffed by veteran quality inspectors utilizing sophisticated experimental equipment and advanced testing methods, every vulcanized batch is verified for tensile strength, abrasion resistance, and elongation limits.
Backed by immense technical strength and a comprehensive global after-sales support system, our rubber conveyor solutions power heavy-duty applications across steel, metallurgy, coal mining, cement, power generation, and port logistics.
In the modern industrial landscape, rubber conveyor belts have become the absolute backbone of bulk material transport systems across multiple sectors. From deep underground mining operations extracting raw minerals to expansive port facilities handling millions of tons of cargo annually, heavy-duty rubber belts facilitate the seamless, continuous movement of essential materials that power our global economy. The evolution of these critical components reflects decades of engineering innovation, advanced polymer science breakthroughs, and an unwavering commitment to operational efficiency, energy conservation, and workplace safety.
Global industrial procurement managers face mounting pressures: minimizing operational downtime, handling highly abrasive or corrosive materials, and complying with stringent environmental and safety standards. As a leading China Conveyor Rubber Supplier & Factories leader, Boao provides holistic macro solutions. Whether supplying multi-ply layered nylon belts (NN, EP), steel wire rope core belts for high-tension long-distance conveying, or specialized heat-resistant and acid-alkali resistant variants, our product lines are engineered to endure extreme operating conditions without premature failure.
Skip the hassle of sourcing from multiple suppliers – our factory provides your ideal packaging and service solutions all in one place. Our technical service plan spans planned replacement, preventative repair, periodic inspection and maintenance, and emergency on-site repair of conveyor belts. By guaranteeing safety stock levels to match your production cadence, managing daily inventory storage, and executing professional vulcanized bonding, we maximize the operational efficiency of your belt conveyors while lowering your total lifecycle cost.
Comprehensive product lineup tailored for diverse industrial sectors requiring robust material handling reliability.
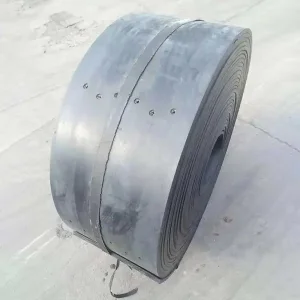
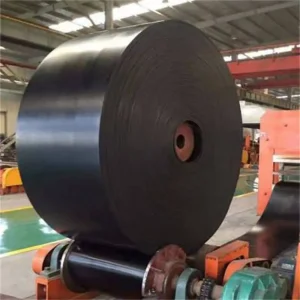
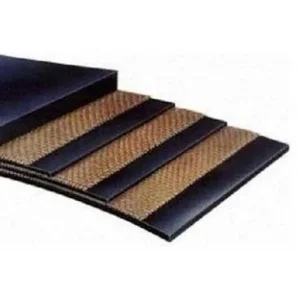
Ordinary conveyor belts (NN, EP, PP), multi-ply fabric belts, high-strength nylon rubber belts, and bulk material handling solutions designed for high tensile performance.
Heat-resistant belts, high-temperature resistant variants, cold-resistant belts, oil & alkali resistant belts, and acid-alkali resistant belts engineered for extreme chemical and thermal environments.
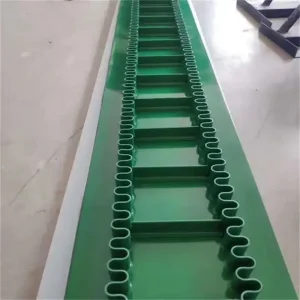
Patterned conveyor belts (herringbone, pit, magic carpet, concave, and convex designs), high inclination belts, wavy edge skirted belts, and rubber waterstop belts.
Anti-tear steel wire rope core conveyor belts for long-distance heavy haulage, and specialized rubber lifting conveyor belts optimized for industrial bucket elevators.
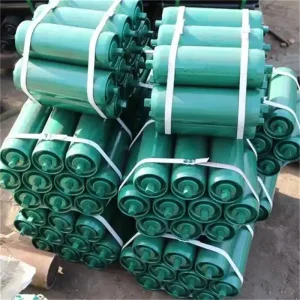
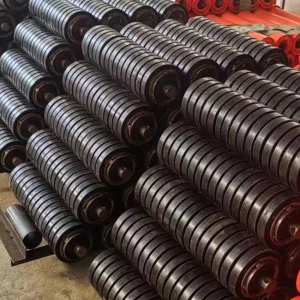
Suspended idler rollers, ceramic rollers, rubber buffer impact rollers, roller groups, electric rollers, rubber-coated rollers, transmission rollers, and strong magnetic rollers.
Trough brackets, centering brackets, tensioning brackets, lifting ears, and heavy-duty structural framework accessories ensuring flawless alignment.
As industry 4.0 integrates smart sensors and automated diagnostics into mechanical systems, the future of conveyor rubber technology lies in predictive maintenance and intelligent compounds. Embedded RFID tracking chips and wear-monitoring conductive rubber layers are becoming standard specs for mission-critical operations. Boao’s R&D roadmap focuses on developing eco-friendly polymer blends that reduce rolling resistance—directly lowering carbon emissions and electricity consumption for industrial end-users worldwide.
Reliability in heavy industry is non-negotiable. Our manufacturing processes strictly adhere to international benchmark certifications (ISO9001 and industry-specific safety standards). By enforcing stringent laboratory testing protocols for tensile tear propagation, flame retardancy, and antistatic properties, Boao guarantees that every meter of conveyor rubber leaving our facility meets or exceeds the regulatory demands of global markets across North America, Europe, Southeast Asia, and South America.
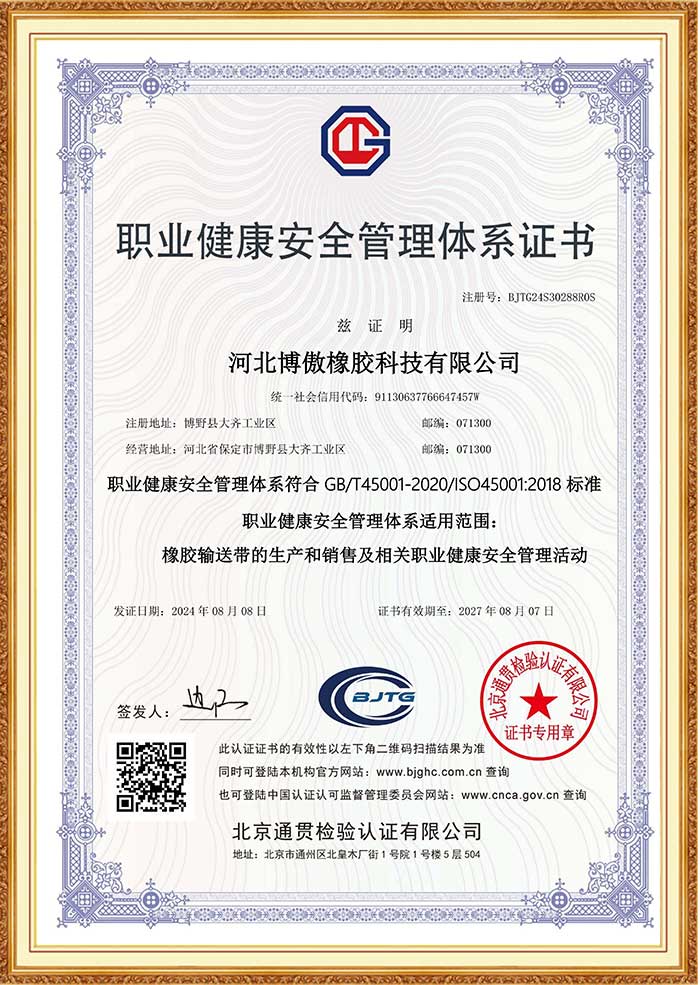
ISO Quality Management
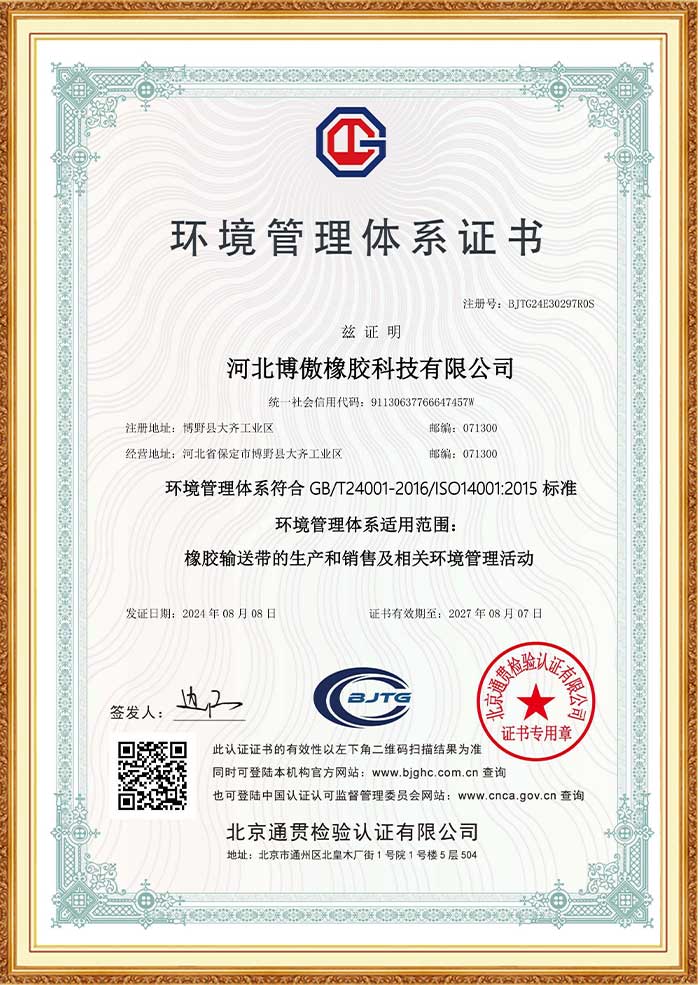
Safety Standard Compliance
Industry Accreditation
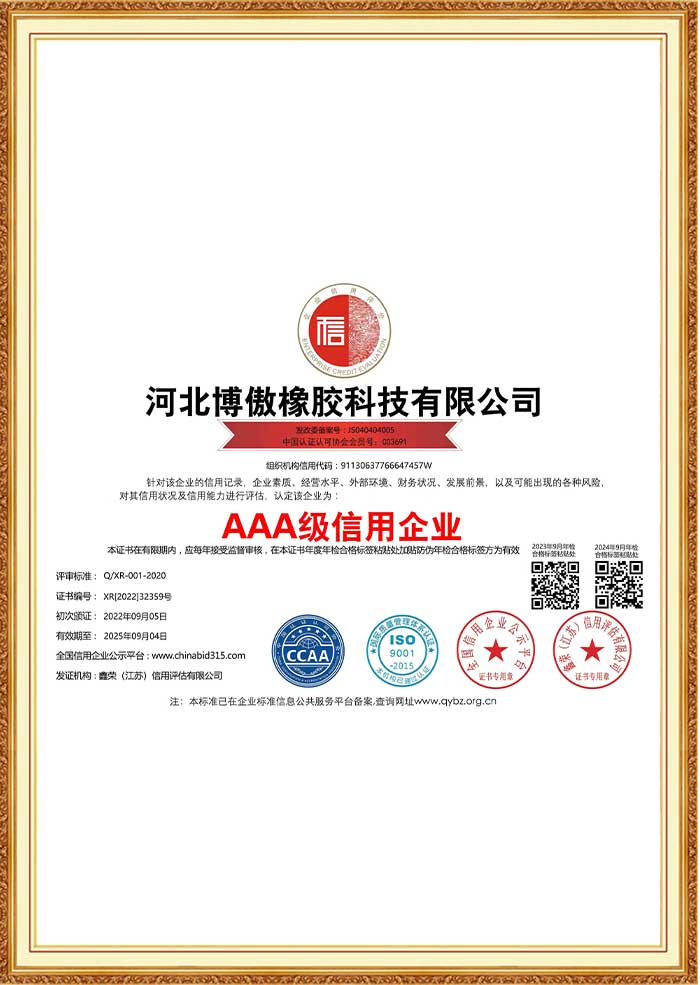
Environmental Verification
Long-term strategic partnerships powering key infrastructure, mining, and metallurgy projects worldwide.
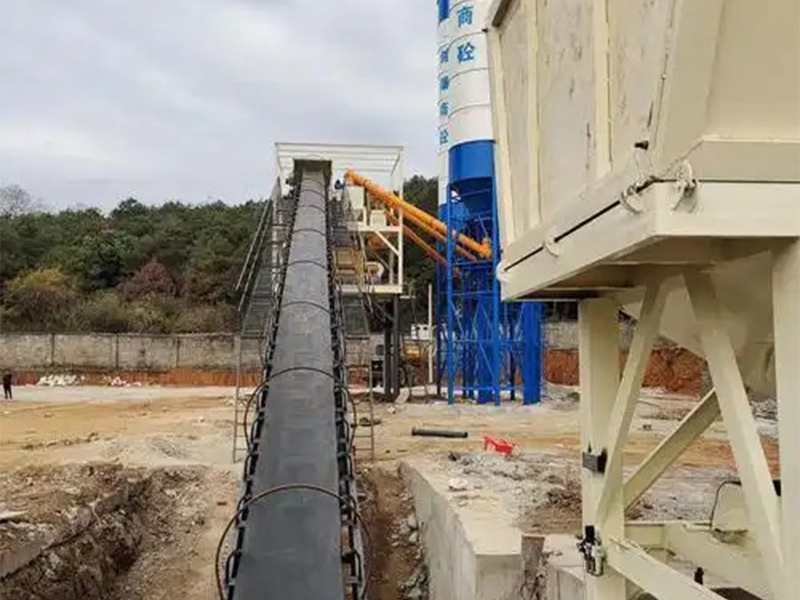
China Railway Group Mixing Plant
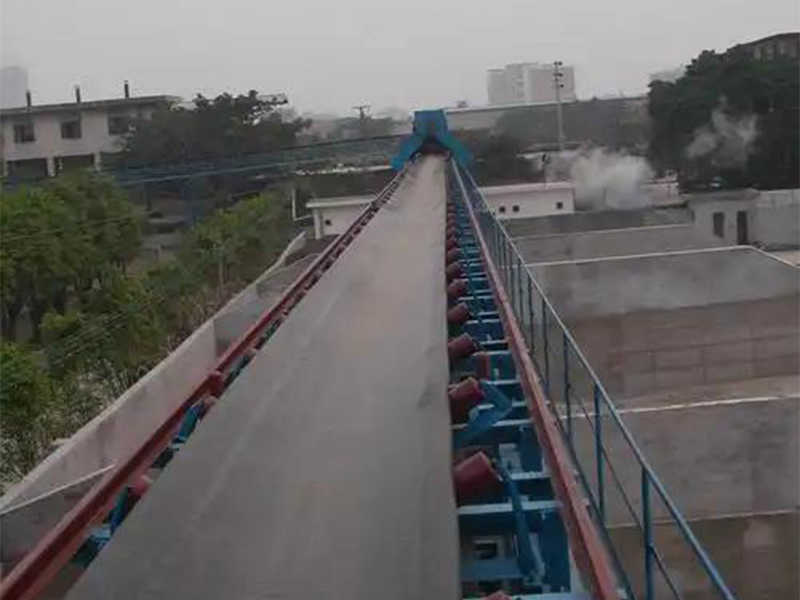
Conch Cement
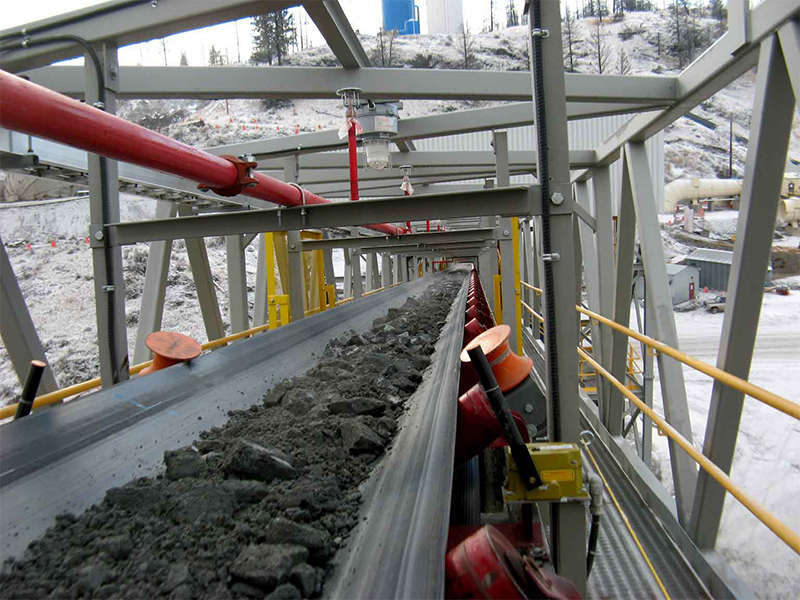
Datong Coal Group
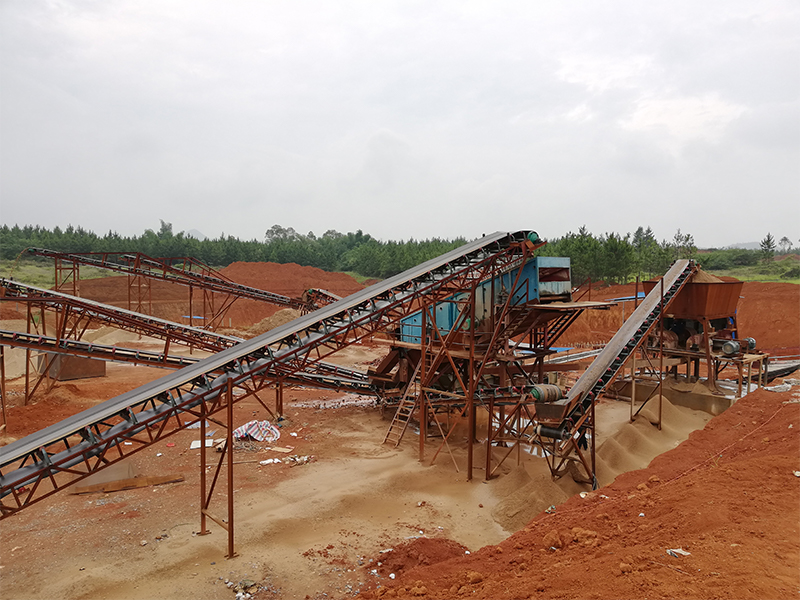
Tsingshan Group
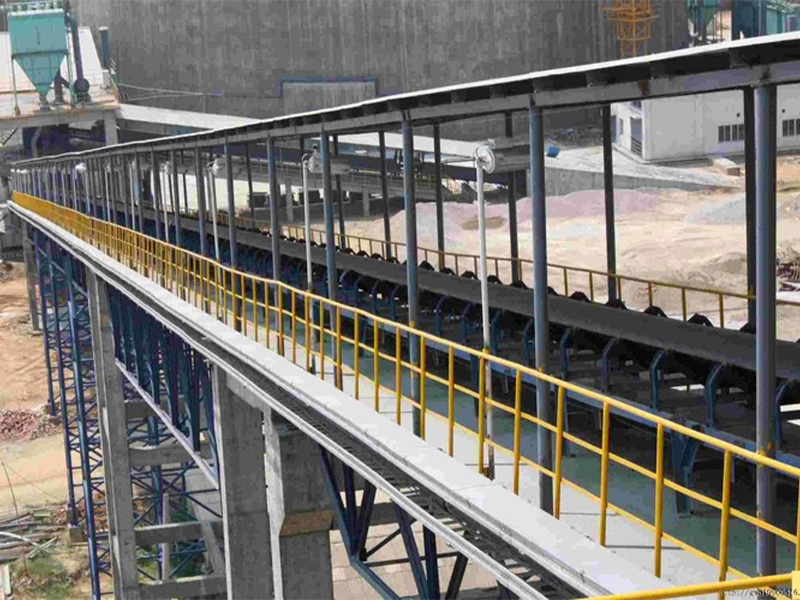
Jidong Cement Group
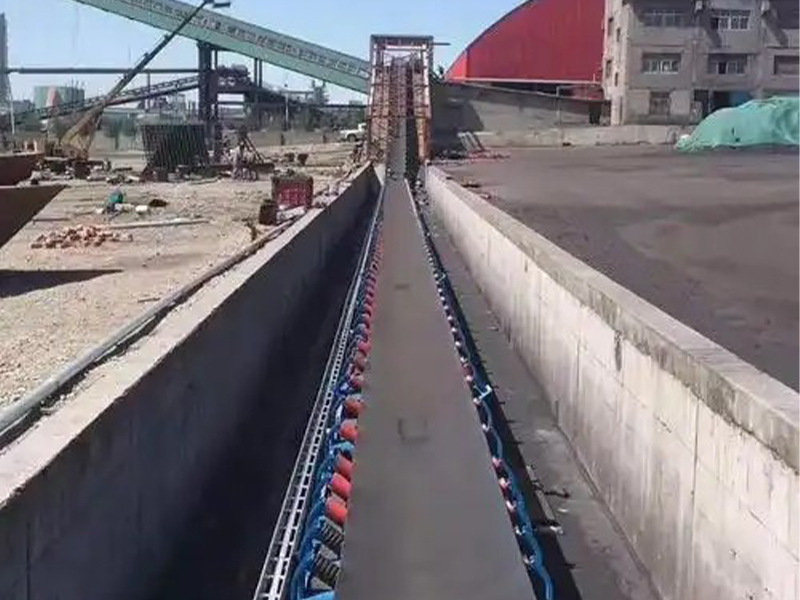
Jinmei Group Coal Conveying Line
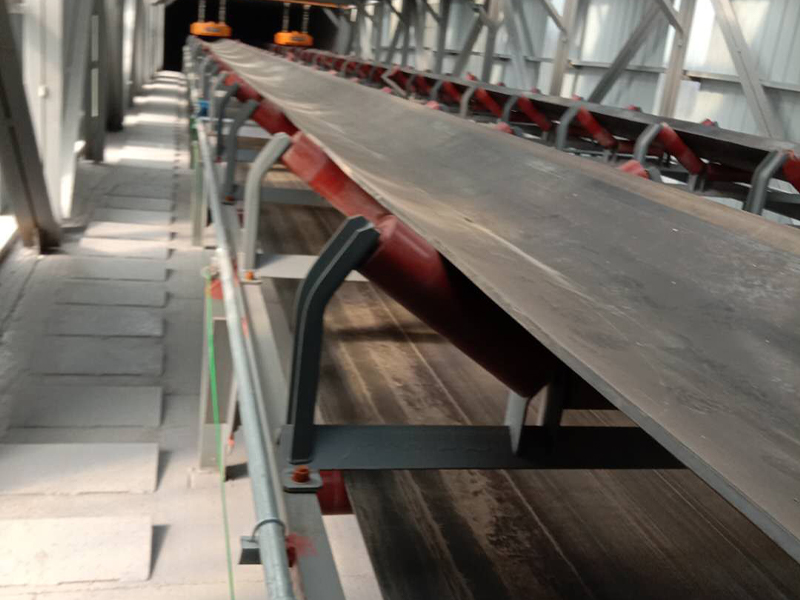
Taihang Steel
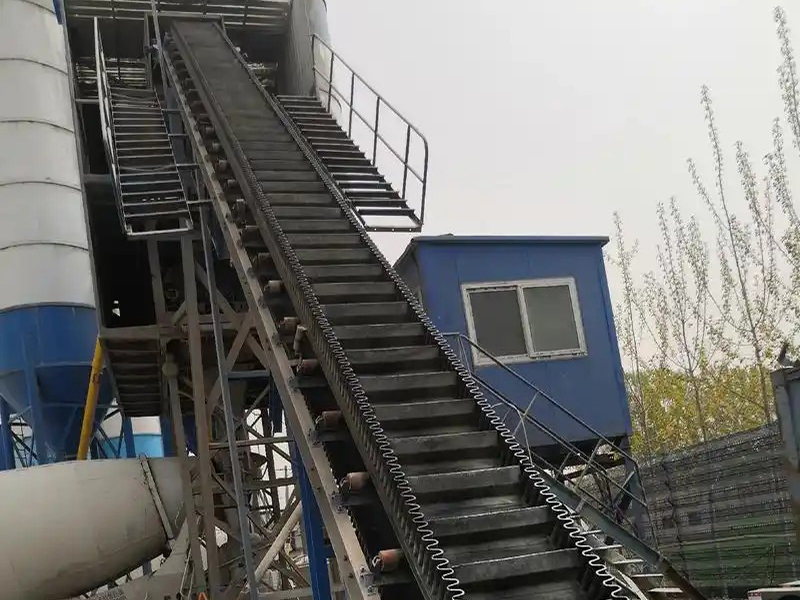
Puyang Steel Group
Expert insights addressing common technical and commercial queries for international conveyor rubber procurement.
EP (Polyester-Polyester) belts feature low elongation, high dimensional stability, and excellent wet-strength, making them ideal for long-distance high-tension runs. NN (Nylon-Nylon) belts offer superior elasticity, exceptional shock absorption, and high impact resistance, perfect for short-to-medium distance material handling with heavy drop impacts.
As a direct manufacturer, we offer comprehensive customization including belt width, carcass tensile strength (EP100 to EP500+), top/bottom rubber cover thickness, specialized rubber compounds (heat, oil, cold, acid/alkali resistance), and customized edge sealing or patterned cleats.
Every batch undergoes strict physical testing in our independent laboratory, measuring tensile strength, elongation at break, abrasion loss (DIN test), adhesion strength between plies, and aging resistance under thermal conditions to guarantee field reliability.
Yes. Beyond supplying world-class conveyor belts and idler rollers, our technical service team provides comprehensive lifecycle management including planned replacement, vulcanized splicing, safety stock auditing, and emergency repair operations.
Explore additional specialized rubber belts, idler rollers, and chemical-resistant conveying systems direct from our factory.
 Boao Rubber