Engineered to withstand extreme tension, high temperatures, and abrasive environments across global mineral processing and transport plants.
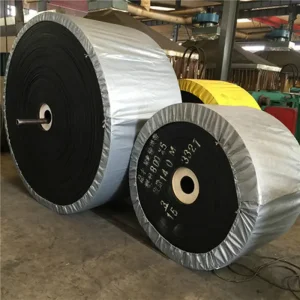
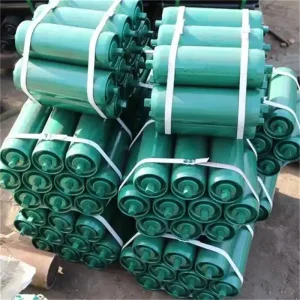
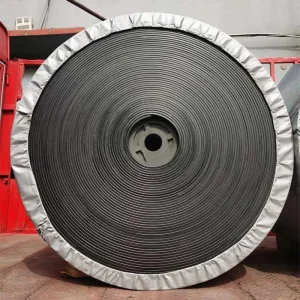
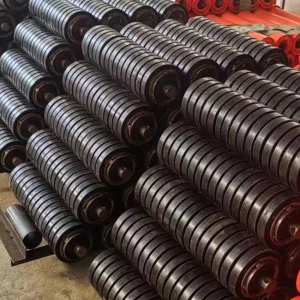
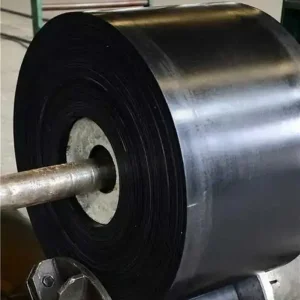
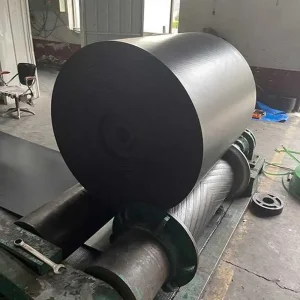
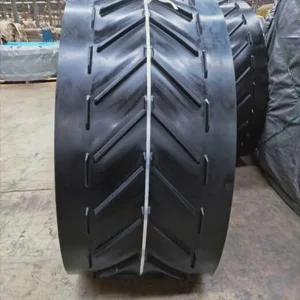
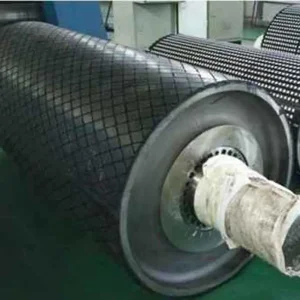
In the modern landscape of smart manufacturing, extraction, and logistics, raw materials are transport lifebloods. As mining depths exceed traditional limits and environmental legislation gets exponentially more demanding, the technology behind material transport systems has transformed. The global market is witnessing an accelerating shift toward closed conveyor systems, widely known as pipe or barrel conveyors, as well as highly specialized heavy-duty fabric and steel-cord belts. These systems offer dustless material transport, low carbon footprint metrics, and optimized structural envelopes.
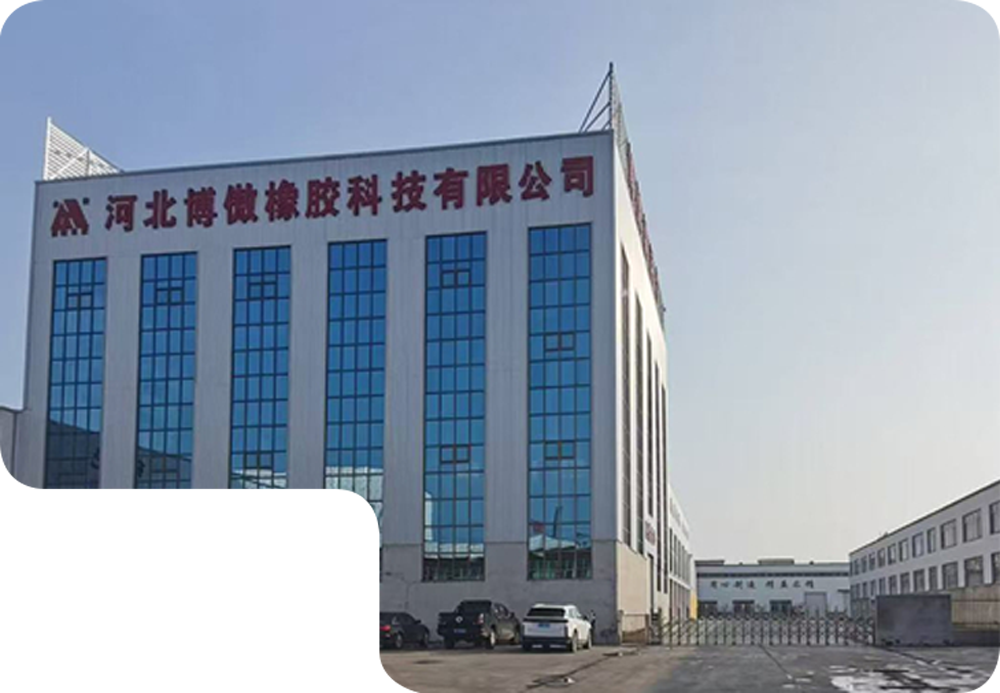
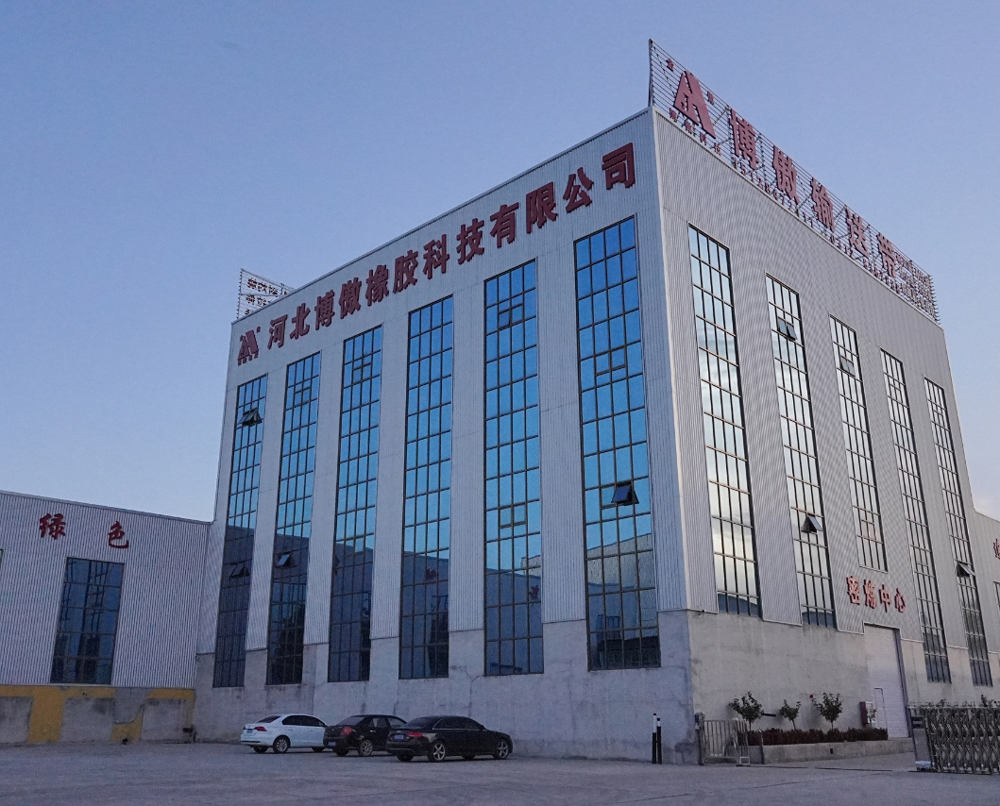
Hebei Boao Rubber Technology Co., Ltd. stands at the intersection of high-polymer material science and mechanical automation. Positioned within the Boye Rubber Industrial Park in Hebei, our production complex addresses this exact industrial evolution. By utilizing automated compounding, continuous vulcanization lines, and real-time physical testing labs, we deliver heavy-duty conveying systems that achieve optimal power consumption, superior tracking characteristics, and high resistance to wear, heat, chemicals, and cold.
Hebei Boao Rubber Technology Co., Ltd. — Pioneers in Industrial Polymer Engineering.
Established in 2004, Hebei Boao Rubber Technology Co., Ltd. has developed into a premier domestic manufacturer integrating product design, polymer synthesis R&D, vulcanization engineering, and comprehensive post-installation systems support. We operate under our flagship brand, "Jinao", which has earned a reputation for reliability in severe-duty material handling applications.
Our state-of-the-art facilities located in Boye County, Baoding, Hebei Province, host specialized machinery for rubber mixing, fabric ply calendering, continuous curing, and dynamic belt fatigue assessment. Our testing labs run round-the-clock chemical checks on raw materials, ensuring that only certified compounds enter our production line.
 Jinao Brand: Over Two Decades of Uncompromised Durability
How Hebei Boao Rubber maintains zero-failure rates in heavy transport lines globally.
We boast an independent analysis laboratory testing incoming carbon blacks, synthetic rubber polymers, fabrics, and steel cords. No raw materials enter production without strict compound sign-offs.
Our quality control inspectors utilize precision laser thickness gauges, tensile testers, and fatigue testing rigs to monitor continuous inline vulcanization, meeting ISO and DIN standards.
Boao belts operate efficiently across the world's most heavy-duty infrastructure networks: from local coal terminals in Shanxi to metallurgical processing complexes across Asia and Europe.
An in-depth whitepaper breakdown of rubber compounds and structural reinforcement properties.
Conveyor belt carcasses bear the mechanical tension of conveying system operations. Choosing the proper material directly dictates resistance to elongation, impact absorption, and structural flexibility. Our design solutions specialize in four carcass classifications:
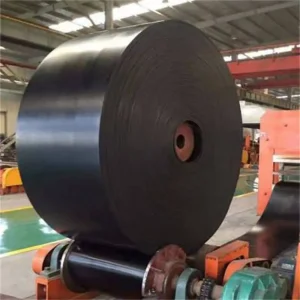
Constructed with polyester warp and polyamide weft plies, EP fabric belts exhibit exceptionally low structural elongation, high tensile strength, and excellent moisture resistance. This configuration makes them ideal for medium-to-long distance applications handling abrasive bulk materials like slag, coal clinker, and aggregate.
Featuring nylon fibers in both warp and weft directions, NN belts offer extreme elastic resilience, superb impact resistance, and maximum fatigue flex life. They are particularly suited for high-impact transition zones, coal drop zones, and steep vertical bucket elevator lines.
Our chemical engineering department develops specialized elastomer polymers to withstand extreme structural stressors:
High tension textile structures for versatile horizontal bulk transport applications.
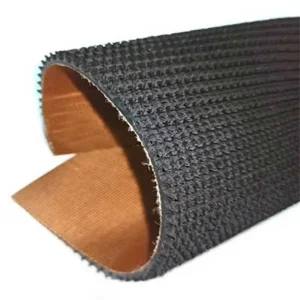
Form-fitting rubber patterns and profiles designed for steep elevation angles.
Precision mechanical rollers and structural brackets to sustain correct tracking.
Demonstrated operational efficiency across major mineral processing and infrastructure corporations.
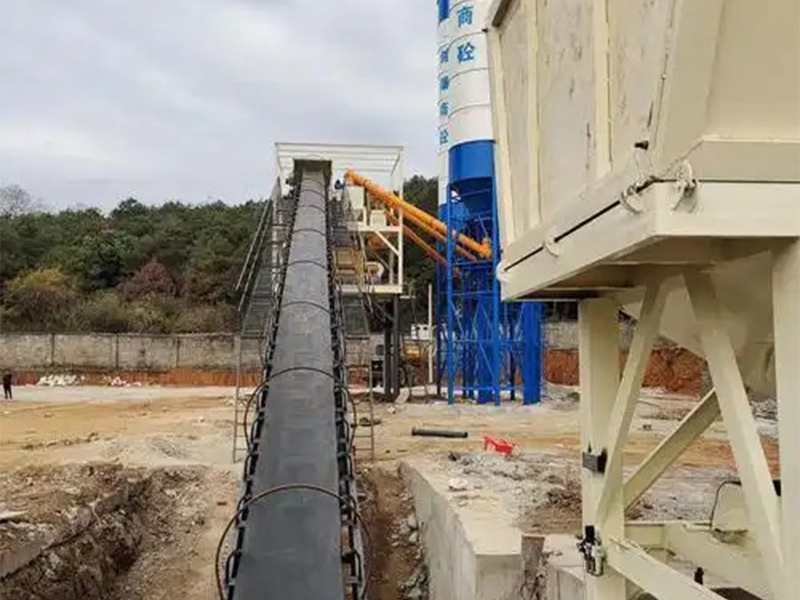
Heavy-duty corrugated sidewall conveyor belts designed for tight spatial aggregate lifting in urban railway systems.
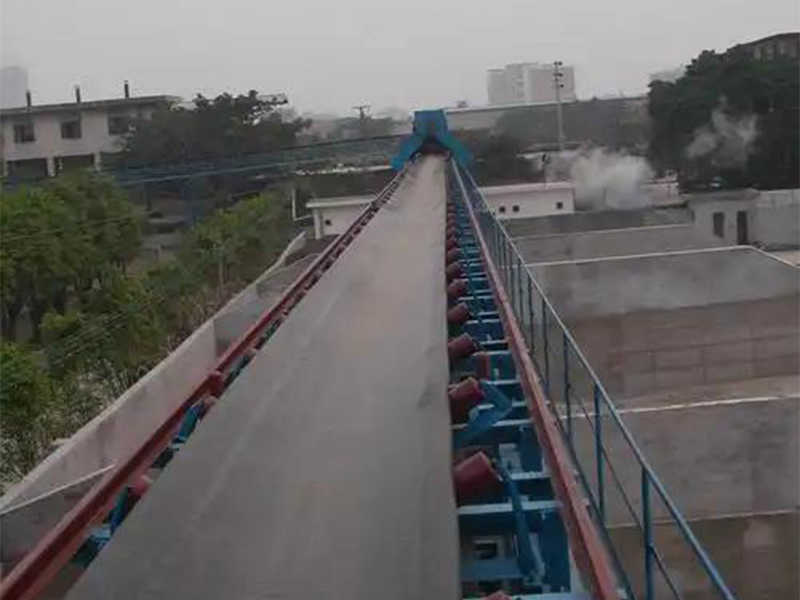
High-temperature resistant EPDM fabric belts transporting hot clinker directly from rotary kilns to silo storage units.
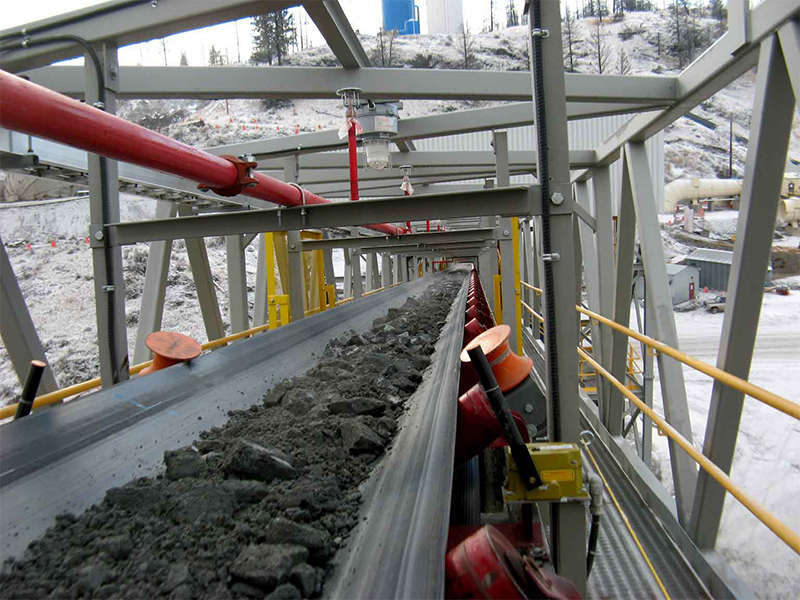
Flame retardant, high-strength steel cord belting with high-impact idler groups for underground logistics corridors.
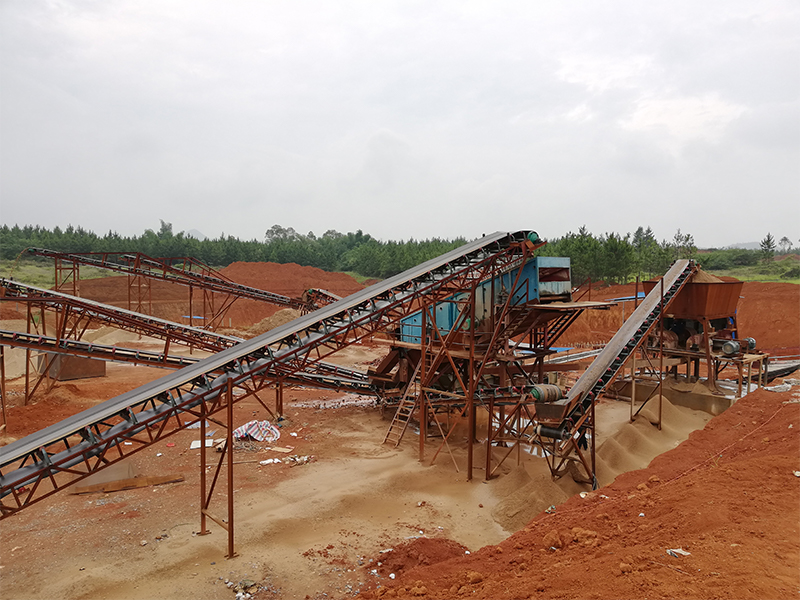
Acid, alkali, and thermal resistant belts designed to sustain uptime on raw mineral feed lines and smelting units.
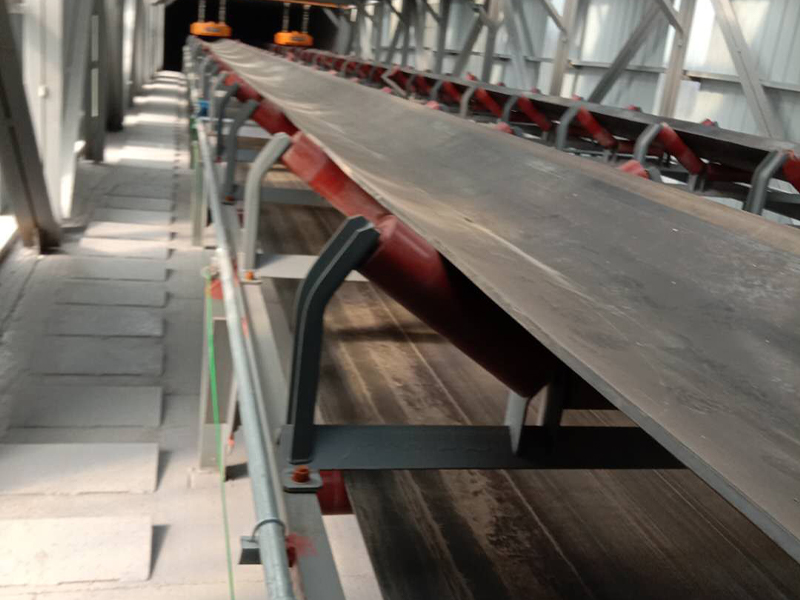
High durability wear-resistant covers designed to process sharp-edged coke and iron ores under dry, high-abrasion parameters.
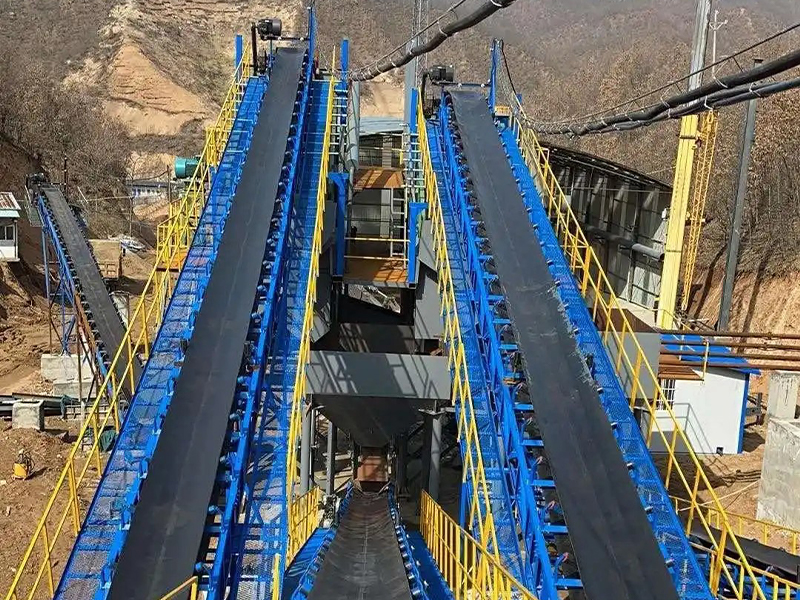
Reinforced nylon belts transporting rough copper and gold ores over long distances, with integrated impact idlers.
Engineered to satisfy stringent global structural, mechanical, and safety regulations.
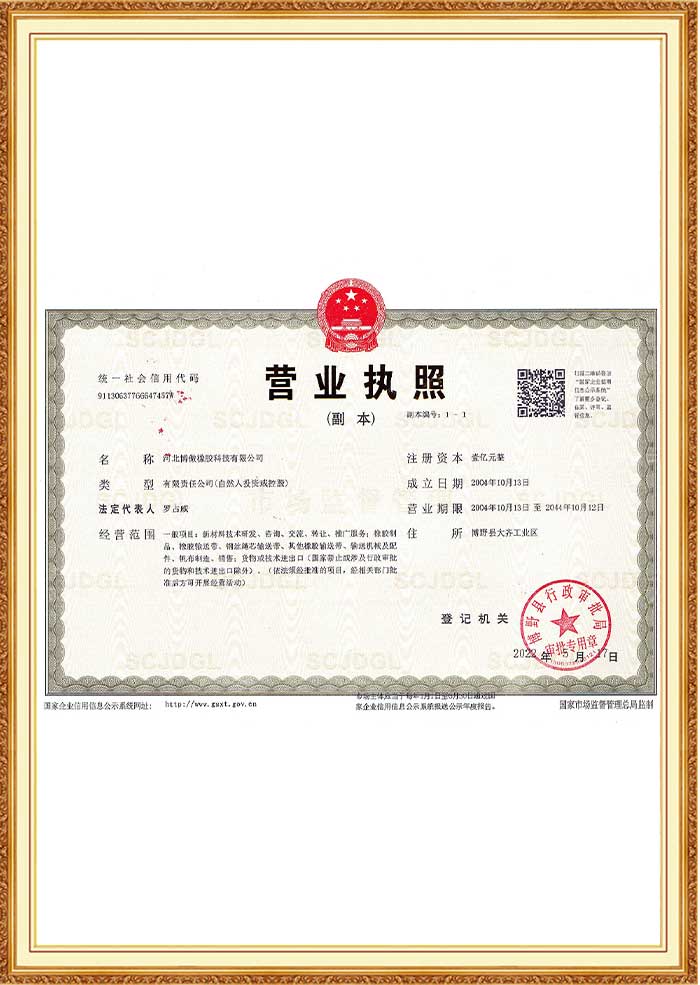
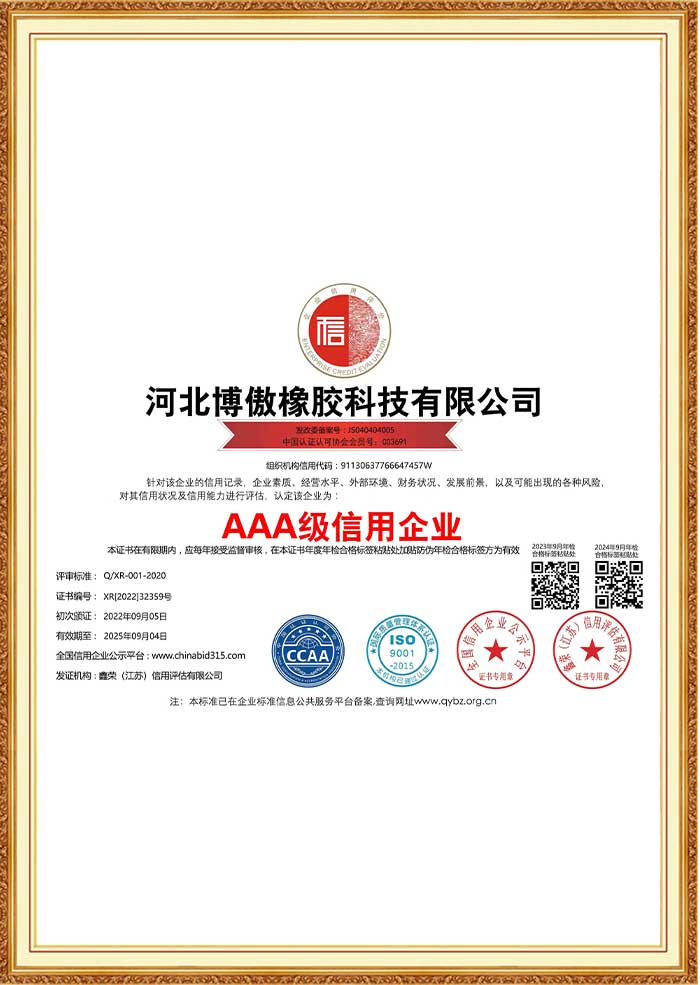
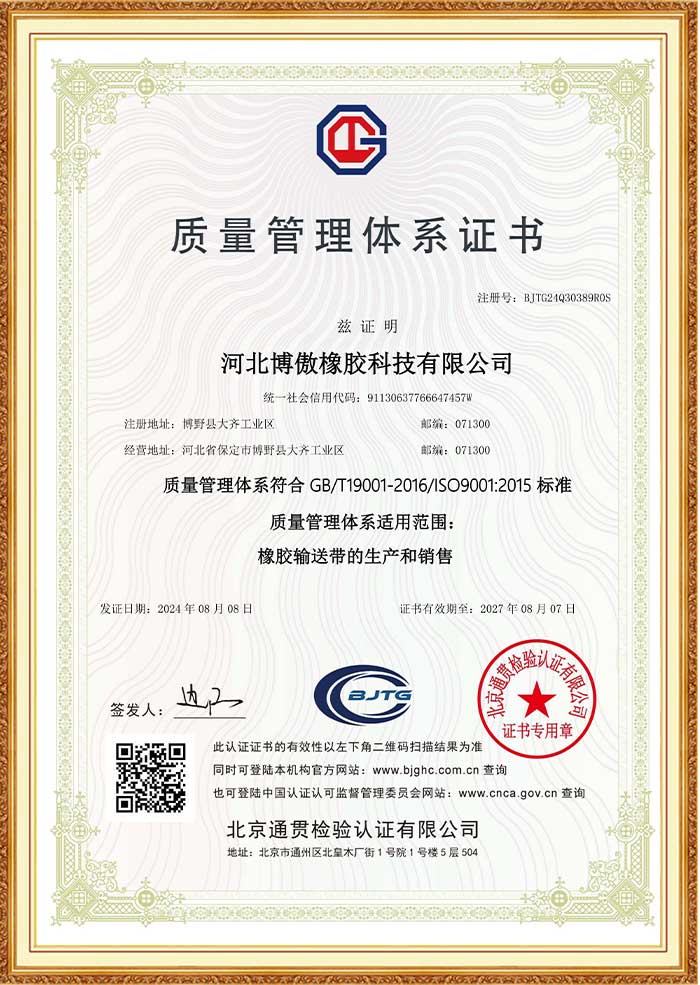
To ensure complete reliability in global chemical, metallurgical, and safety-critical projects, our manufacturing lines strictly adhere to international certifications, including ISO 9001 and high-grade safety certificates for coal mine applications.
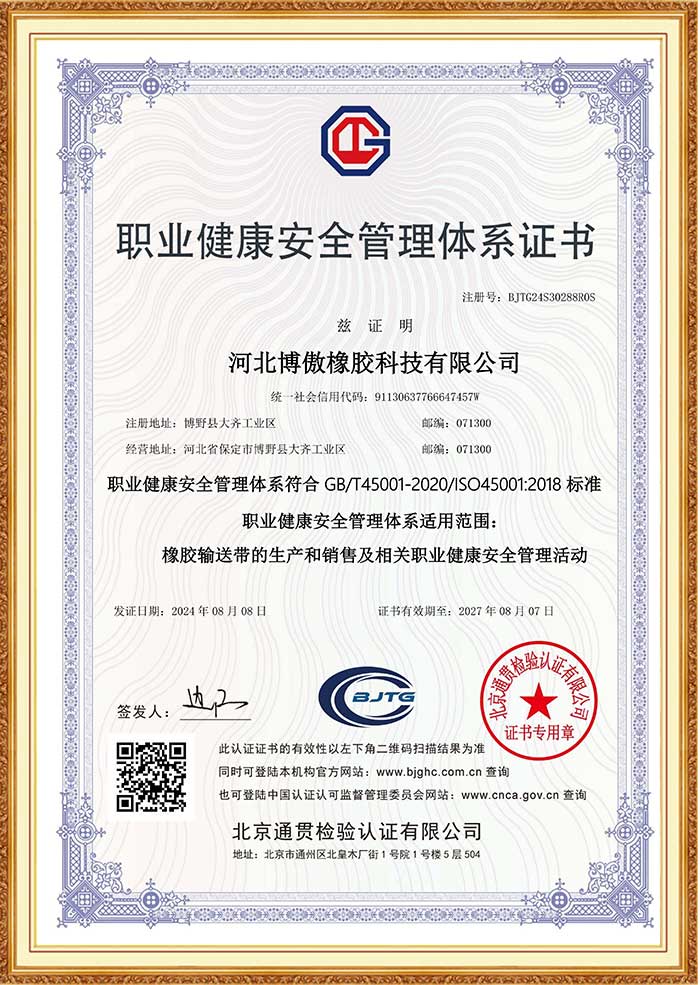
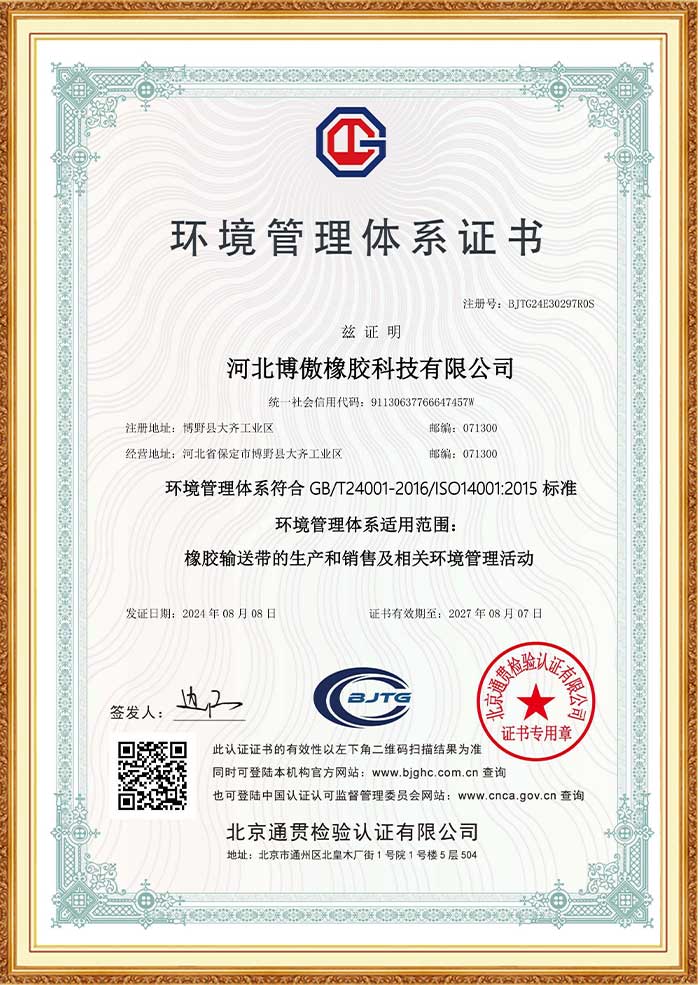
Comprehensive after-sales service and scheduled preventative maintenance for heavy transport systems.
Preventative site inspections, planned structural replacements, hot/cold splice joints vulcanization, and emergency belt repairs.
Supply of custom-formulated splice materials, dynamic inventory tracking to maintain client safety stock, cover repairs, and site idler alignment audits.
Optimizing conveyor tracking, reducing drive power load, extending the lifespan of conveyor belts, and maintaining zero-dust sealing standards.
We coordinate routine site visits to monitor wear rates, perform safety checks, and help clients lower their total cost of ownership (TCO).
The next generation of bulk handling requires a focus on energy consumption and system intelligence. Over 60% of a long-distance conveyor's carbon footprint stems from indentation rolling resistance (IRR) between the belt cover and support rollers. Our technology roadmap addresses these environmental demands:
By developing rubber matrices that combine specialized synthetic elastomers with modified carbon black structures, we reduce energy loss during belt compression over idlers. Under test conditions, Jinao LRR belts decrease motor power draw by 12% to 18%, saving operational costs on long-distance overland runs.
Integrating passive RFID chips and vulcanized copper sensor loops into steel cord matrices enables automated conveyor systems to monitor cover wear and splice elongation. If a longitudinal tear occurs, sensor loops communicate with control modules to halt the line, preventing catastrophic damage.
Professional technical answers to help engineering procurement managers specify material transport systems.
Explore our full catalog of durable fabric belts, steel cord belts, and precision idlers manufactured under strict quality standards.
Get in touch with our design engineers for customized rubber compounding, belt tension calculations, and structural layouts. We offer comprehensive quoting for international shipping and commissioning services.
Submit RFQ / Inquiry Boao Rubber