Explore our industrial-grade, certified conveyor belts and accessories designed for extreme environments, heavy abrasion, and long-range transport.
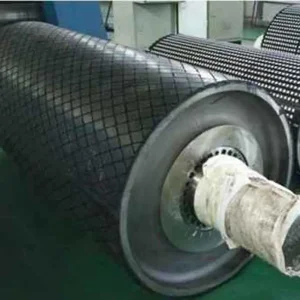
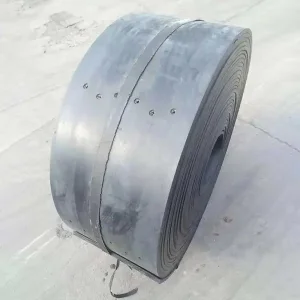
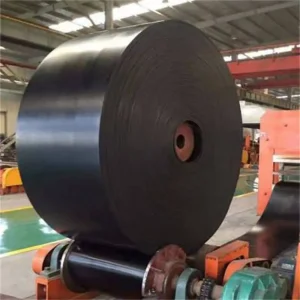
Bridging raw materials extraction and modern processing with resilient elastomer transport systems.
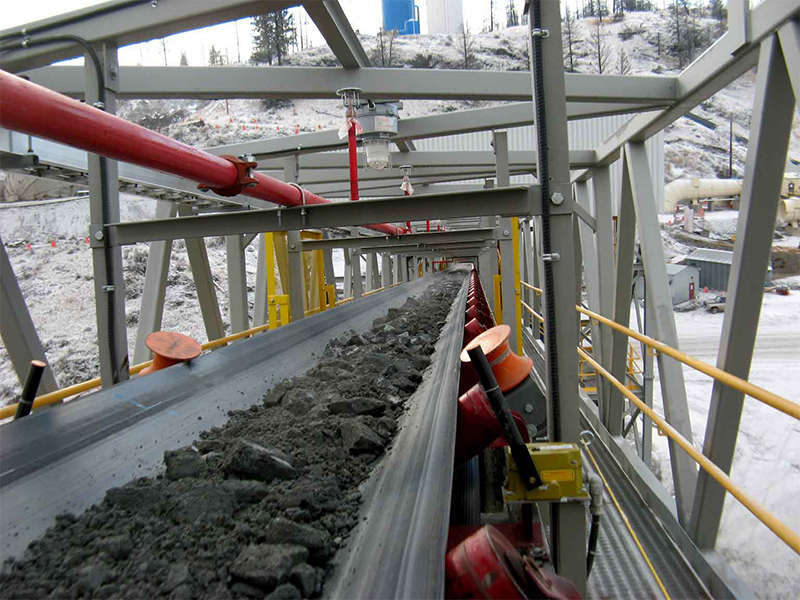
Globally, industrial rubber conveyor belts serve as the foundational arteries of heavy industry. From deep underground coal mines in North America to mega-ports handling metallurgical ores in Western Australia, the efficiency of dry bulk handling depends heavily on conveyor belt durability. As global supply chains demand higher throughput, industries are moving away from traditional mechanical trucking to continuous conveyor loops, reducing greenhouse gas emissions and operational bottlenecks.
With the rapid expansion of international mining and green cement production, conveyor belts must survive extreme conditions—whether operating in Siberian temperatures of -50°C or handling hot clinker at temperatures exceeding 200°C. Heavy industries rely on specialized engineering formulations to balance tensile strength, impact absorption, and elastic longevity.
A 22-year legacy of engineering reliable "Jinao" brand products under stringent quality frameworks.
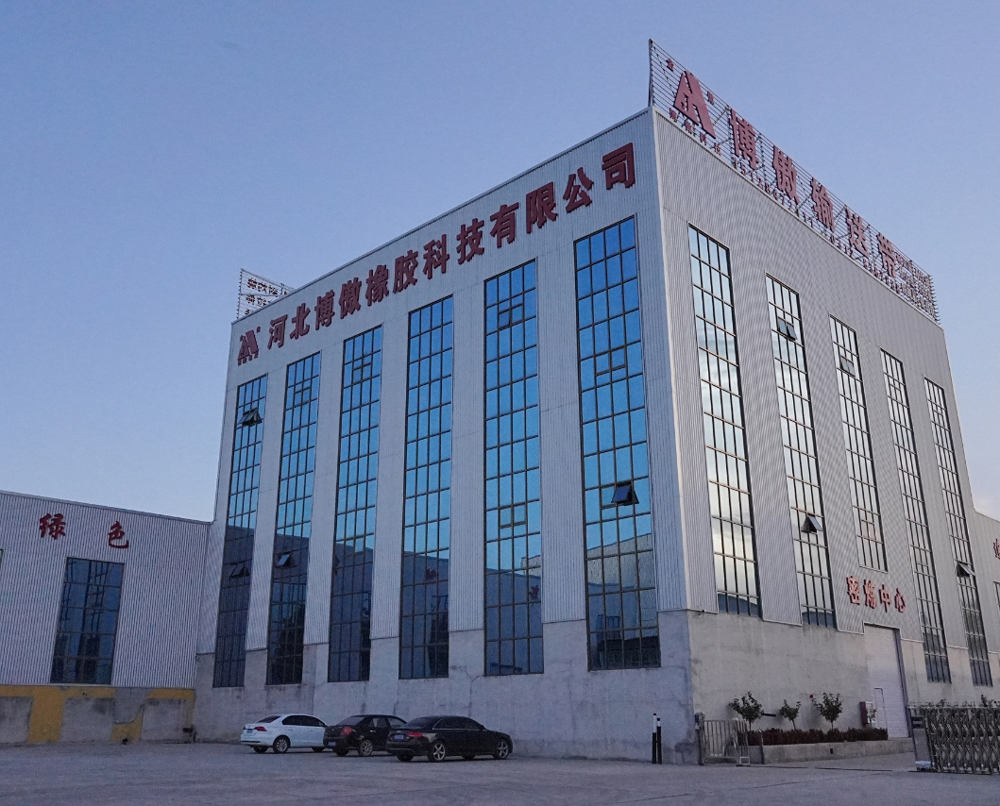
Established in 2004, Hebei Boao Rubber Technology Co., Ltd. sits in the heart of the boye county Rubber Industrial Park in Baoding, Hebei, China. Occupying over 30 acres of advanced manufacturing space, our facility integrates high-precision polymer research, customized product design, and strict quality control. Our signature brand, Jinao, has become synonymous with durability, safety, and performance.
Equipped with state-of-the-art production lines for calender rolling, compounding, molding, vulcanization, and material analysis, we cover the entire product lifecycle—from raw elastomer input to finished product compliance testing. Our operations adhere strictly to international quality management system certifications, ensuring every shipment complies with DIN, AS, ISO, and SANS global metrics.
Our operational capabilities translate directly into physical metrics, engineering advantages, and absolute reliability for your conveying needs.
We build systems designed to operate without interruptions, safeguarding your material flows and minimizing downtime through rigorous engineering and testing.
Featuring independent chemical analysis rooms and physical test laboratories, our quality control team checks every phase—from raw polymer and wire cord receipt to final vulcanized output. Unqualified compounds never enter the shop floor, and non-conforming products never leave our dock.
Equipped with sophisticated ozone testing cabinets, abrasion testers, electronic tensile testing machines, and rubber rheometers, we run dynamic fatigue and adhesion testing to verify product performance in harsh field configurations.
Supported by a comprehensive technical network and local logistics centers, our Jinao products operate across high-intensity sectors like metallurgical mills, thermal coal operations, global logistics ports, municipal mixing hubs, and chemical plants.
Our specialized conveyor belts meet specific application needs, utilizing advanced compounding and reinforcement skeletons.
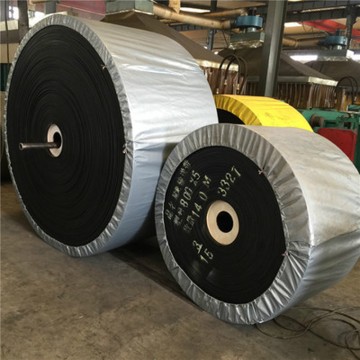
Designed for cement plants, sintering, and fertilizer processing, handling materials up to 400°C with specialty EPDM elastomers.
View Details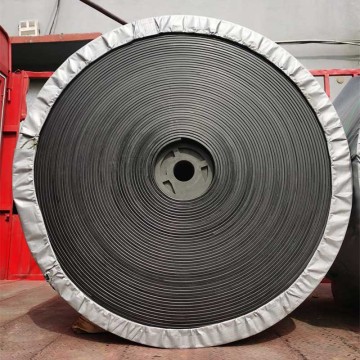
Optimized for sub-zero mining environments, preserving rubber flexibility and crack resistance down to -50°C.
View Details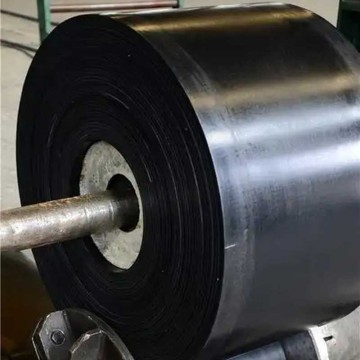
Formulated to resist chemical attacks in fertilizer and metal processing, utilizing corrosion-proof synthetic rubber polymers.
View Details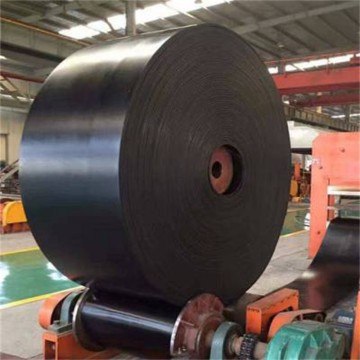
Providing high elasticity, high tensile strength, and excellent impact absorption for mid-to-long distance conveying systems.
View Details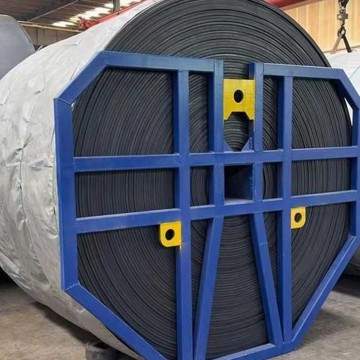
Reinforced with high-tensile steel cords, built for overland bulk transport and high-load mining environments.
View Details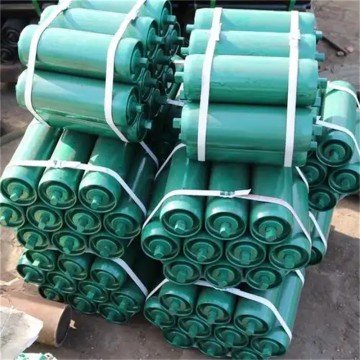
Engineered to minimize friction, lower system power needs, and protect the belt carcass at critical loading points.
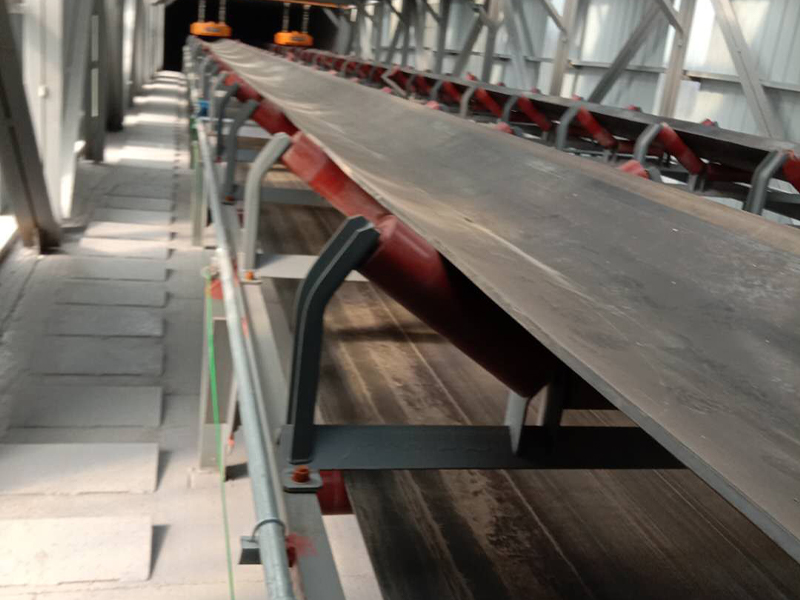
View DetailsFrom ore extraction to energy distribution, Jinao conveyor systems keep heavy industries running efficiently.
Beyond supplying hardware, we deliver complete technical support to optimize belt lifespans and ensure safe operations.
Our engineers analyze your load patterns, material abrasiveness, drop-height metrics, and structural layouts to recommend the correct rubber compound and carcass thickness.
We calculate dynamic splice efficiency and drive power needs based on ISO 5048 and DIN standards, optimizing the safety factor to reduce drive energy consumption.
We supply premium hot/cold vulcanizing materials, bonding agents, and detailed instructions to make sure splices match the strength of the main belt carcass.
Our services include real-time wear-indicator tracking, planned rubber cover maintenance, and prompt replacement components to help prevent costly unexpected shutdowns.
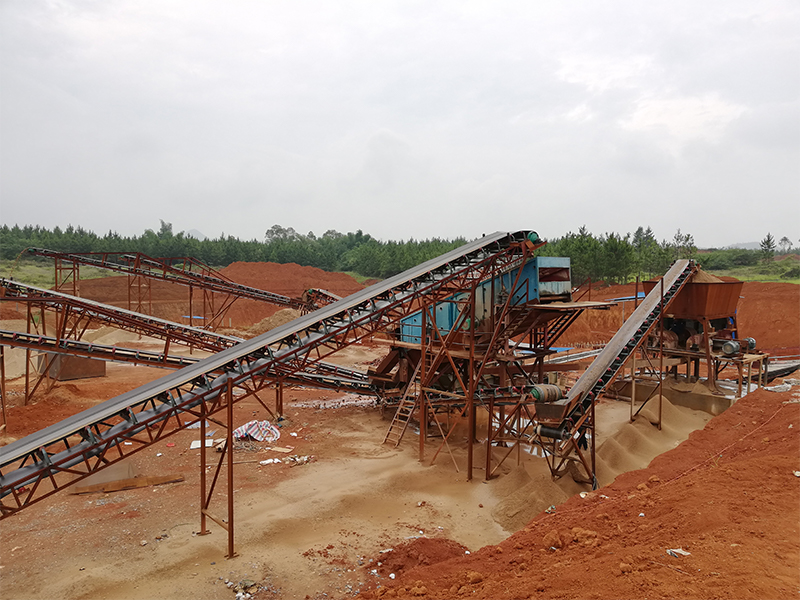
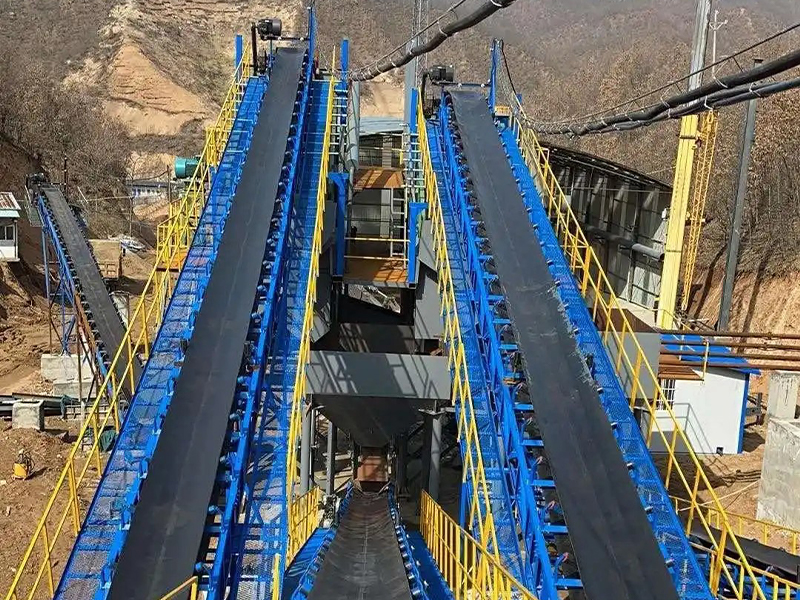
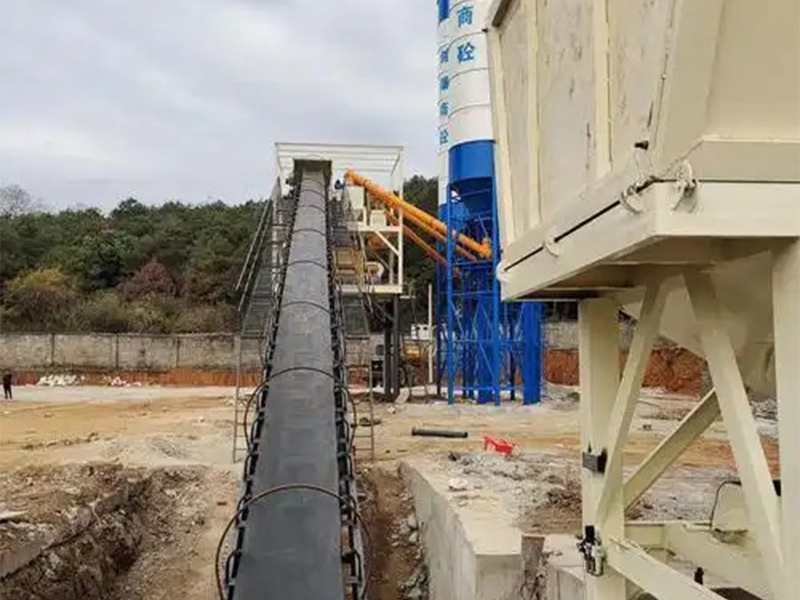
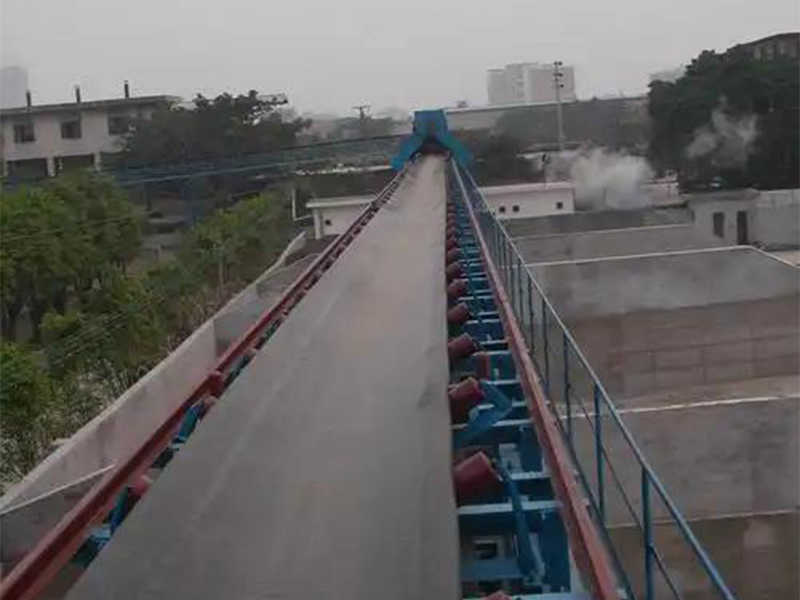
Our conveyor solutions support critical industrial processes across leading resource, logistics, and steel corporations.
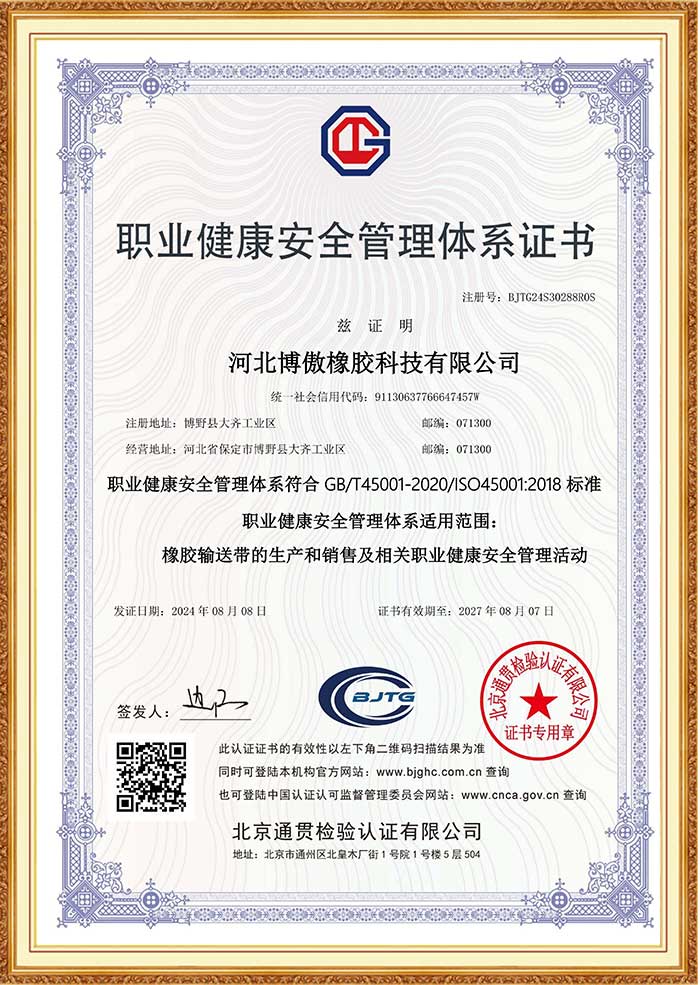
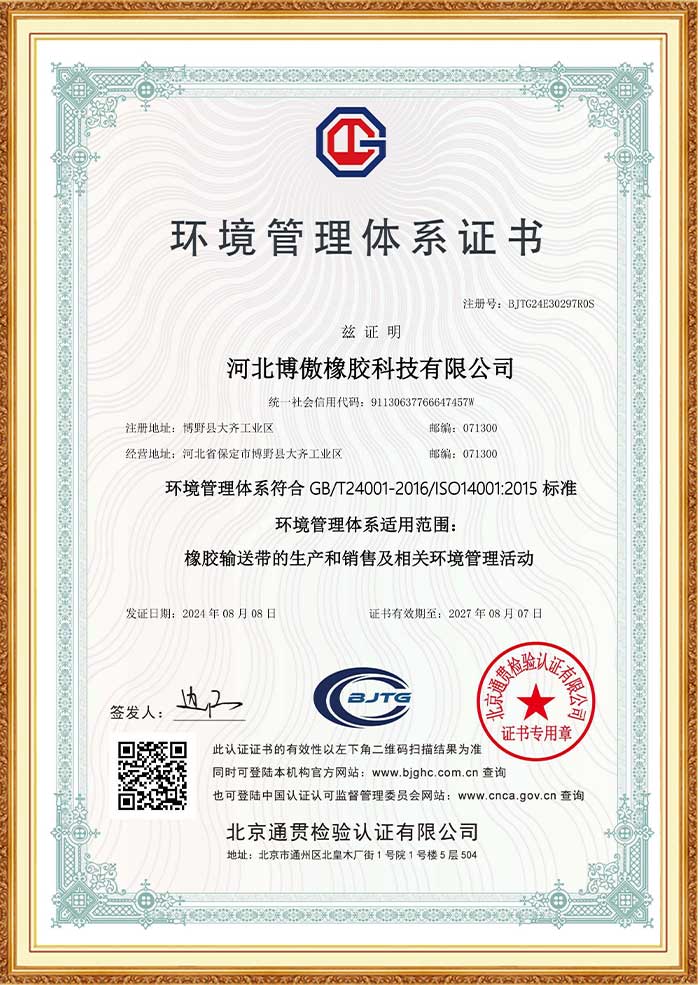
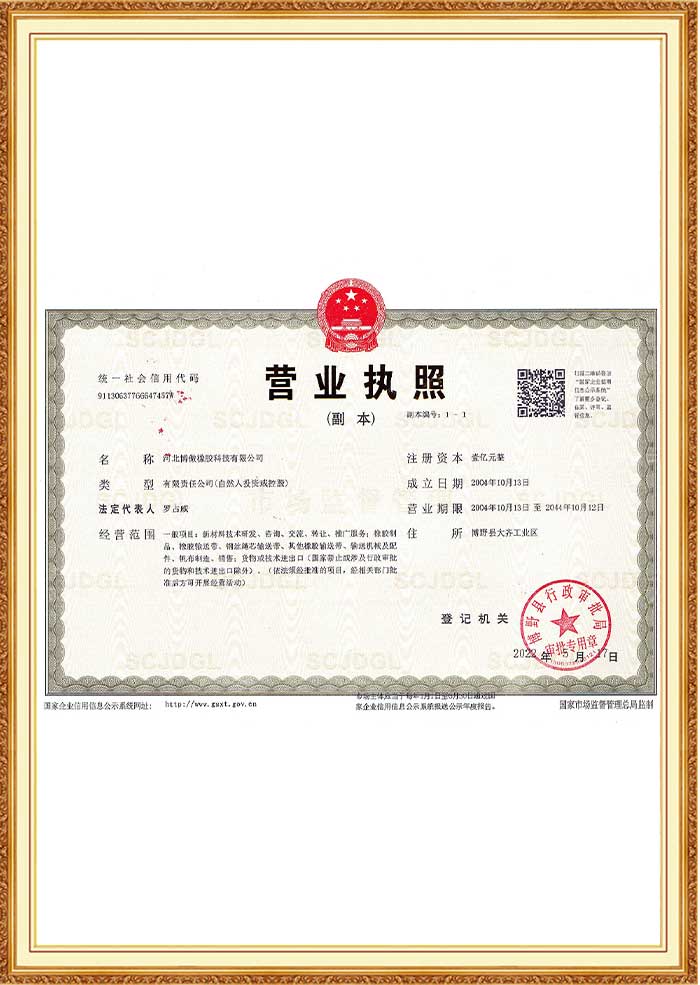
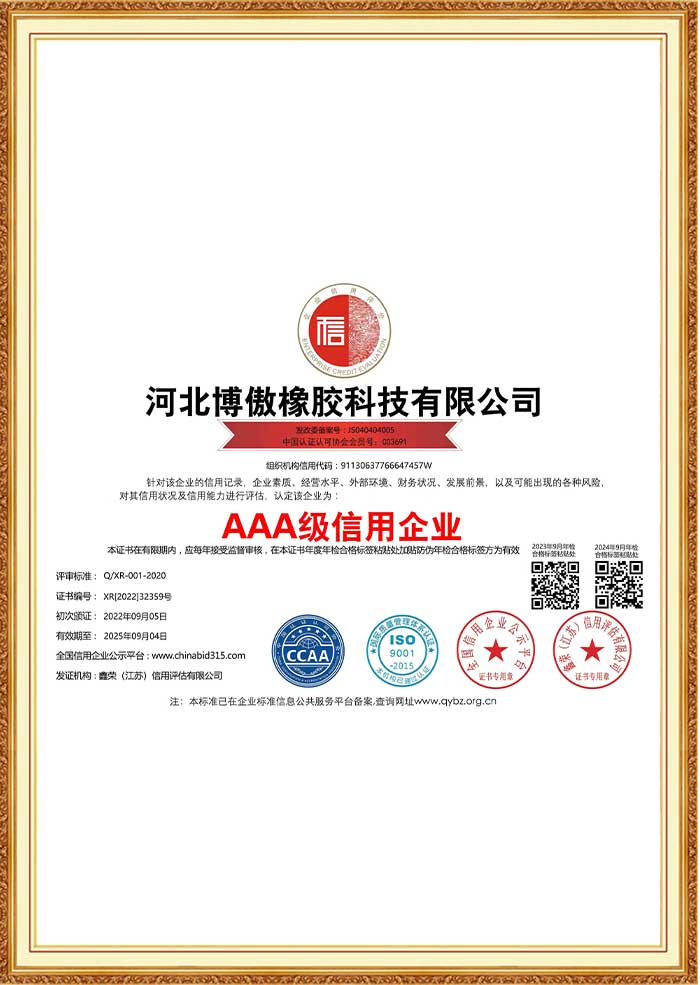
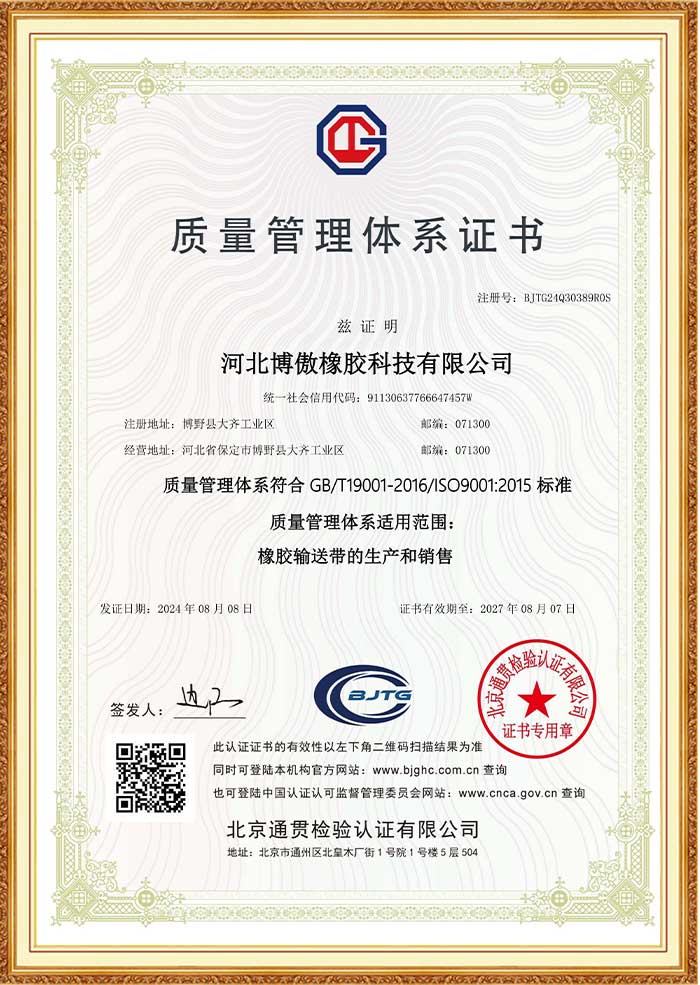
Our quality management systems and industrial products are fully certified, ensuring they meet rigorous international performance standards.
Find answers to common engineering questions regarding belt selection, rubber compound performance, and preventative maintenance.
EP (Polyester-Nylon) belts provide high tensile strength, minimal elongation under load, and excellent resistance to water and rot, making them ideal for long-distance conveyor systems. NN (Nylon-Nylon) belts offer superior elasticity, excellent shock absorption, and high flexibility, which makes them well-suited for high-impact loading zones and deep troughing systems.
For temperatures from 120°C up to 400°C, we recommend our specialized Heat-Resistant (HR) belts. These are formulated with EPDM or chlorobutadiene elastomers, which resist hardening and cracking caused by prolonged thermal exposure.
Our cold-resistant rubber formulations undergo testing in sub-zero environmental chambers. We test for impact resilience, crack propagation, and flexibility down to -50°C to ensure the belt maintains its physical properties in extreme cold.
We supply high-grade raw splicing rubber and cover compounds that match the vulcanizing parameters of the parent belt. Our detailed installation guides ensure the vulcanized joint achieves maximum durability and strength.
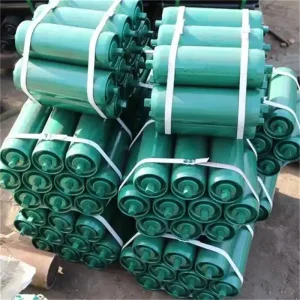
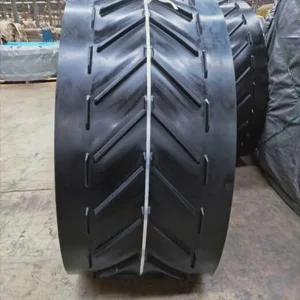
Explore our complete product catalog, featuring heavy-duty steel wire reinforced belts, customized patterns, and high-efficiency idler systems.
Get in touch with our engineering team for custom carcass designs, detailed quote options, and expert on-site technical support.
Request A Quote Boao Rubber