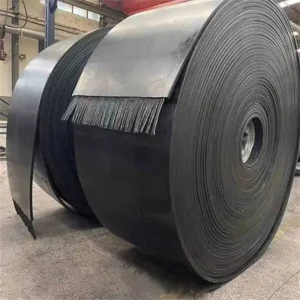
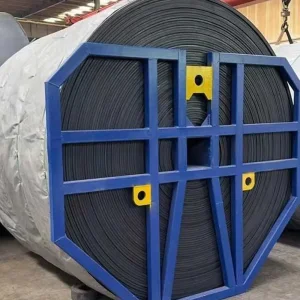
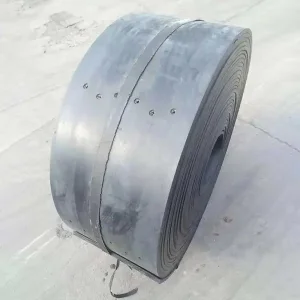
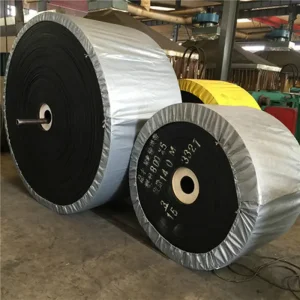
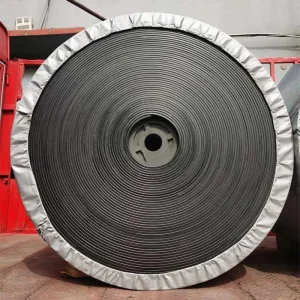
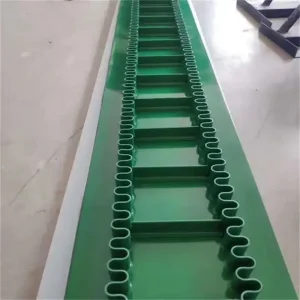
High-performance belts engineered to withstand the demanding humidity, saline conditions, and dynamic loading cycles of Caribbean ports and quarry structures.
The Castries market in Saint Lucia serves as a primary maritime transshipment hub, importing and exporting high volumes of dry bulk materials. The port terminals demand conveyor belt structures that perform optimally under high tension while managing severe environmental stressors. This white paper highlights how steel wire rope core conveyor belts represent the apex of material handling engineering, delivering unmatched longitudinal stability and tear protection.
Traditional textile-reinforced belts fail prematurely in these environments under high-load tensions. High-strength steel wire rope cores, combined with specialized anti-tear transverse networks, are crucial for maintaining continuous runtimes. This reduces unscheduled maintenance and increases port operational efficiency.
As a leading conveyor belt manufacturer, Hebei Boao Rubber Technology Co., Ltd. (producing the renowned Jinao brand) utilizes advanced material science to design industrial-grade conveyor belts. Our engineering targets key performance areas for the Castries industrial market and international distribution channels:
Our galvanized steel cords are designed for high elasticity and fatigue resistance, providing maximum breaking strength and minimal elongation under load.
Built with transverse steel cord reinforcing layers to stop longitudinal slicing from sharp aggregates, rock basalt, and industrial minerals.
Our high-molecular rubber covers are formulated to resist dynamic degradation in tropical marine environments, preventing delamination and core rust.
The manufacturing capabilities of China-based facilities, such as the Hebei Boao Rubber technology park, deliver substantial cost advantages and fast production turnarounds without compromising on quality. Over 30 acres of advanced manufacturing space, equipped with continuous vulcanizing lines and heavy duty testing machinery, enable the production of belts that meet standard tolerances under international certifications like DIN, ISO, and AS.
Our Quality Assurance process includes independent chemical analysis and physical testing labs to ensure every conveyor belt run meets client specifications before shipping to Castries ports or global mining operations.
Providing reliable material handling components to prominent mining, aggregate, and manufacturing operations globally and regionally.
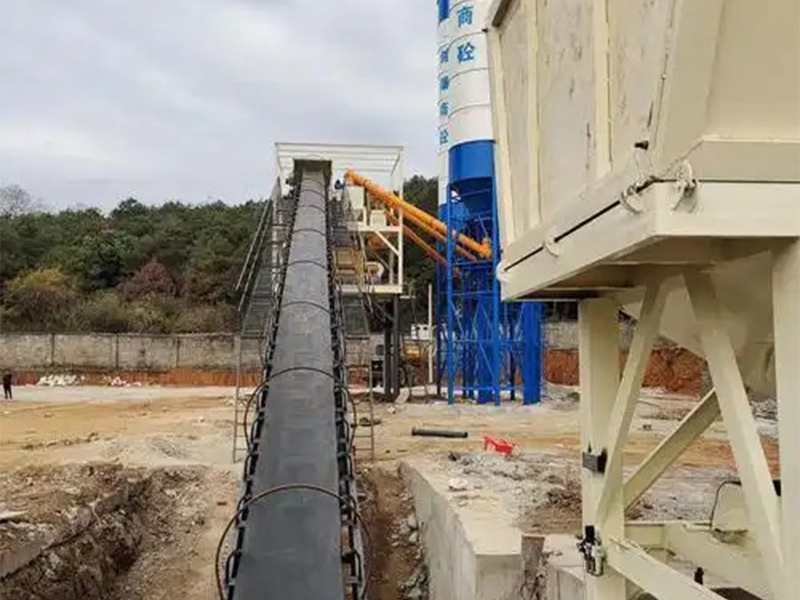
Fitted high-tension steel cord belt systems at deep-water shipping terminals, handling abrasive dry cargo without belt stretch.
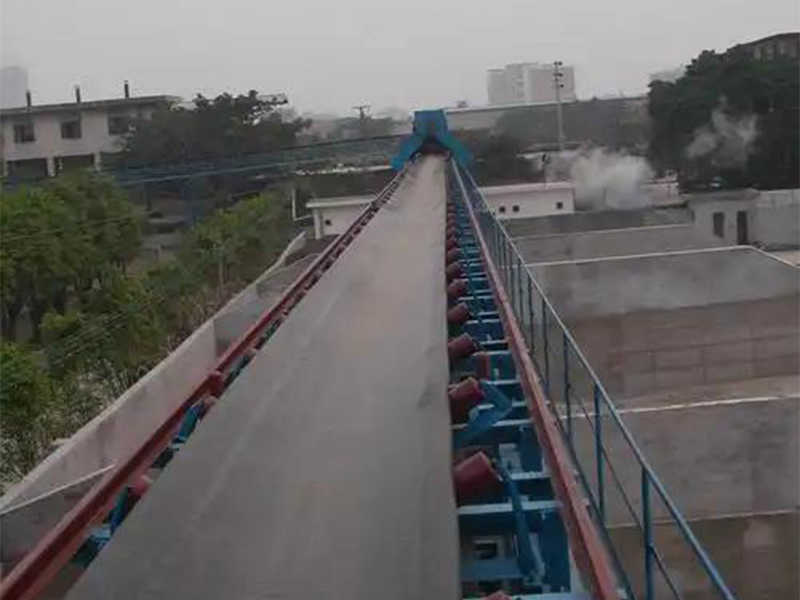
Supplied high-integrity anti-tear steel core belts to run over long-distance aggregate transport corridors under variable loads.
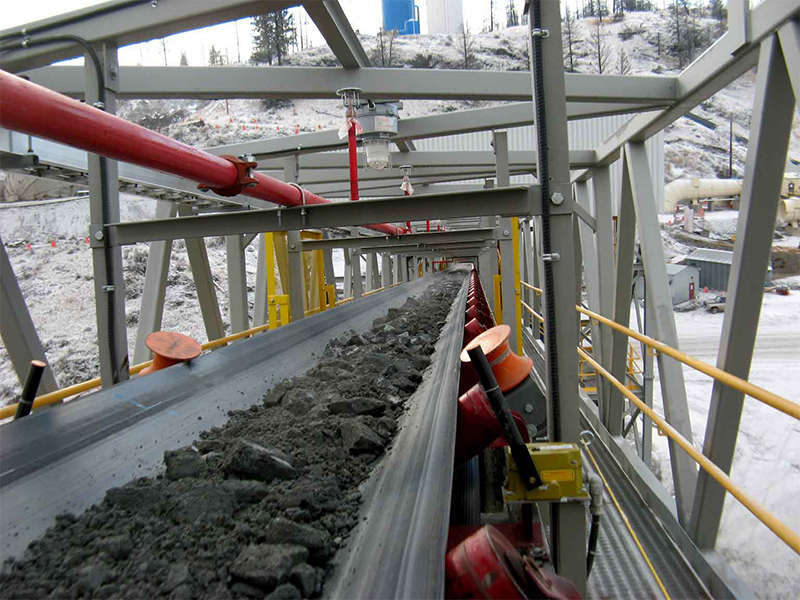
Delivered customized heat and moisture-resistant conveyor systems to handle dynamic cement packing processes in tropical climates.
We work closely with Castries terminal engineers, quarry operators, and global sourcing specialists to ensure every belt meets structural design parameters. Our manufacturing capabilities include:
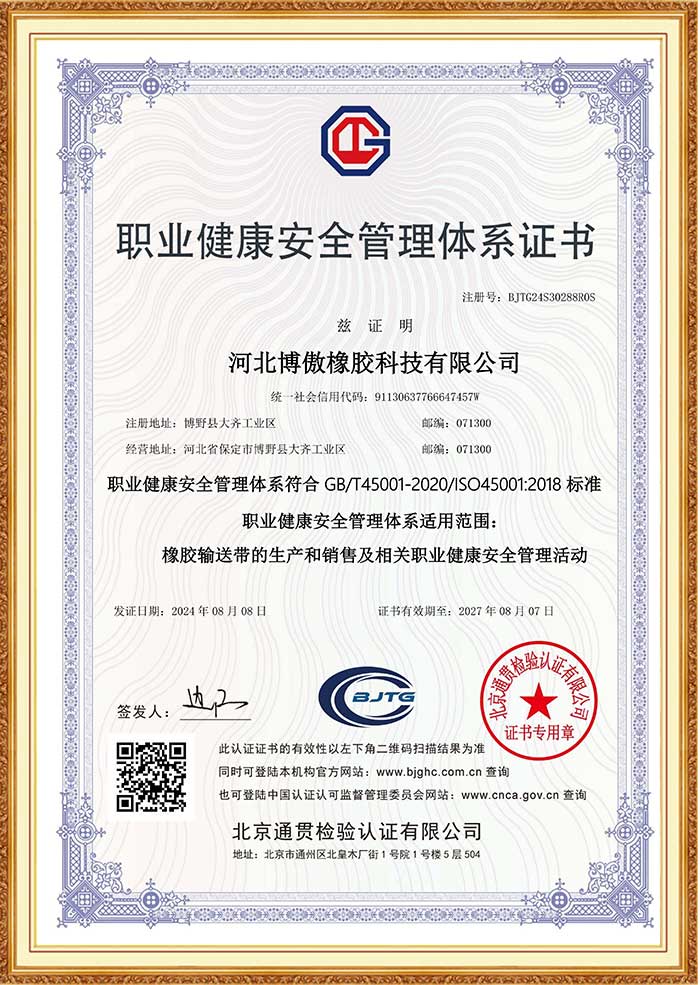
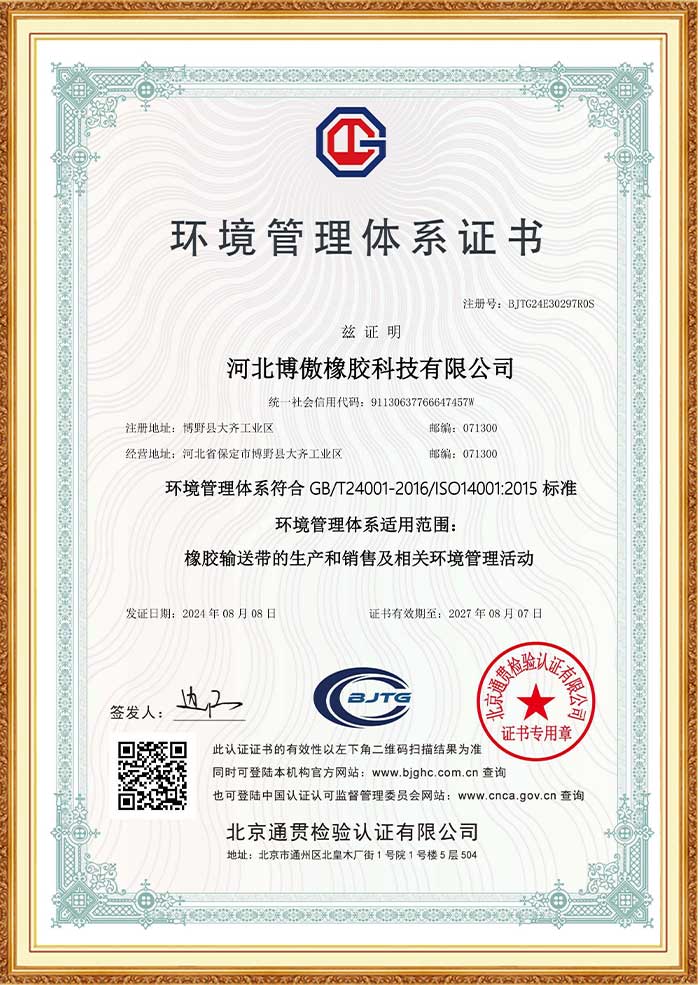
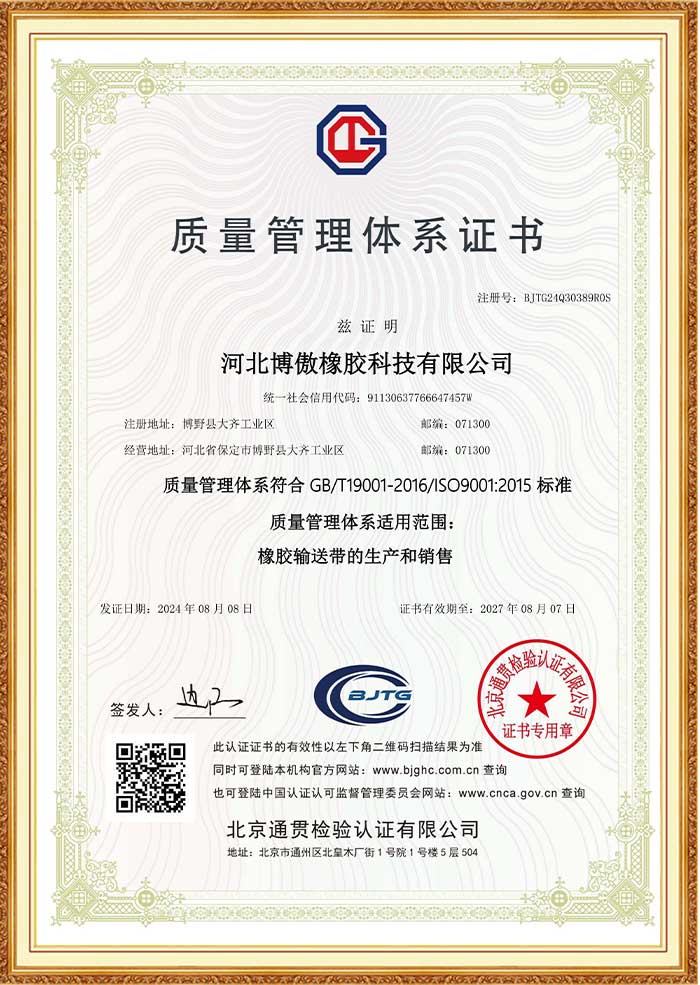
All conveyor systems are manufactured and verified under ISO-certified quality control parameters, ensuring durable operation in demanding working conditions.
Technical explanations and answers to common inquiries from engineers and procurement managers.
High-durability conveyor systems, idler rollers, and components engineered for reliable material handling operations.
Request customized engineering plans, material datasheets, and direct factory pricing. Our logistics network supports direct delivery to port terminals in Castries and global industrial sites.
Send Inquiry Now Boao Rubber